AT A GLANCE:
General information
This section applies to anyone who lifts loads using the crane, performs work on the crane, or works nearby.
At the start
Using this product manual
The following symbols are used in this product manual:
- This is an instruction regarding an action and prompts you to perform a work step.
- This is the result of an action and describes what happens on the device.
- This is a list.
Only with...
A section that appears in a box framed by a dashed line is only applicable for certain types, versions or options. The condition to which the section applies is specified at the beginning in the heading “Only with...”.
Instructions for the product manual
Read the product manual through carefully before beginning work. Also be sure to observe additional product manuals for accessories and components.
Afterwards, keep the product manual available in the vicinity of the crane. It must be accessible to all who work with or on the crane.
In the case of reselling or hiring out, always provide the product manual together with the crane.
If equipment is limited, e.g. the drive or main girder connection plate and screws from ABUS are not included, the corresponding sections in the product manual do not apply.
Note regarding the designation “CRANE”
The product manual assumes that the end carriage is used together with a main girder as a crane. As a result, it uses crane specific terms. Other applications are not ruled out by this and the corresponding instructions apply in the same way.
Proper use
The end carriage travels with both wheels on a crane track or trolley track. It is designed for cranes and trolleys within the maximum load capacity.
- The end carriage travels in an operating range along a crane track or trolley track.
- The end carriage must not collide at high speed with other end carriages on the same crane track or at the crane track end stopper. The redundantly connected crane travel limit switches and redundantly connected anti-collision devices prevent this from happening.
- The end carriage may be operated outdoors if it is appropriately equipped. This includes the openings being properly sealed, the end carriage being appropriately painted, the end carriage having rain hoods, the main girder connection being protected from water ingress and precautions being taken by the end user against dangers from ice, wind, rain, dust and other environmental factors.
See “Equipping the crane for operation in unprotected environments” section in the “General product manual for ABUS cranes”.
- This product manual describes the use, installation, removal and maintenance of the components included such as wheels, crane travel drive, guide rollers, clamping pieces and derailing protection device. It does not include specifications for designing or constructing machines manufactured by you. The end carriages or wheel blocks are not a complete machine. For the limits of their use, please refer to the data sheets or other documentation provided.
- The production tolerances for the manufacturing and installation process and the electrical activation are decisive for the risks and usability. For this reason, the crane's manufacturing tolerances as well as the crane track tolerances must be followed. The user is responsible for this during operation. The end carriages and the wheel blocks have not been subjected to any test load.
- The user must hold welding qualifications of at least level EXC 3 according to DIN EN 1090. Welding on the end carriages may lead to undercuts, which affect anticipated operating times. The user must therefore hold the appropriate qualification for welding dynamically loaded components.
Regulations
The installation has been built and tested according to European standards, rules and regulations applicable at the time of its manufacture. The conventions applied during design and construction are specified in the Declaration of Conformity or the Declaration of Incorporation. The conventions must also be observed for installation, operation, inspection and maintenance, as must the applicable occupational health and safety regulations.
Which provision applies in individual cases will greatly depend on the crane’s use and the national regulations. Review and observe all applicable and current regulations, including the occupational health and safety regulations. Refer also to the Declaration of Conformity or Declaration of Incorporation.
Warranty
- ABUS assumes no liability for damages that were caused by improper use, inadequately trained personnel, incorrect performance of work, nor for any changes, reconstruction or other modification of the crane or crane components which were not approved by ABUS.
- Any warranty claim becomes invalid if components were modified without consent, the crane or crane components were installed, used or serviced in any way other than that described in this product manual, or if parts other than original ABUS replacement parts were used.
- Safe operation of the crane or crane components is only guaranteed if original ABUS replacement parts are used.
The end carriage
End carriage - description of the device
Detailed view of end carriage
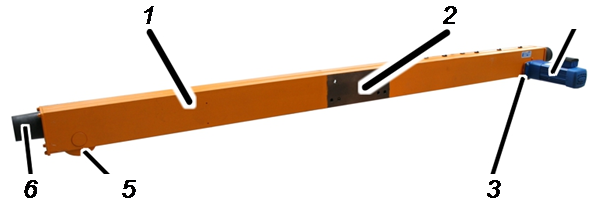
Detailed view of end carriage V500
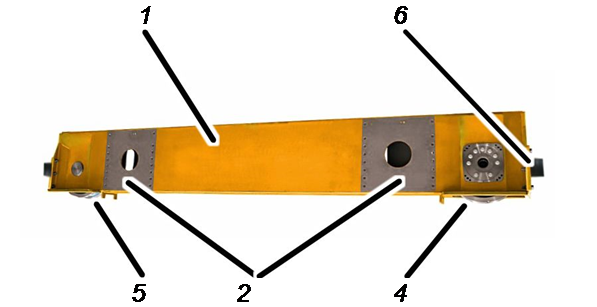
- 1: End carriage
- 2: Joint face
- 3: Crane travel drive
- 4: Wheel, powered
- 5: Wheel, not powered
- 6: Safety buffer
Wheel block - description of the device
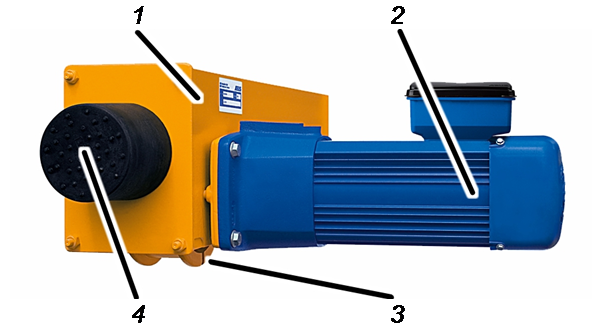
- 1: Wheel block
- 2: Crane travel drive
(AZP version here) - 3: Wheel, powered
- 4: Safety buffer
Performance features
The end carriages:
- The end carriages are fully-automatic, welded box girders.
- The end carriages are connected to the main girders using high-tensile bolts.
- The end carriages (according to the respective width of the crane track) have wheels with wheel flanges, which enable even running on the crane track and prevent the overhead travelling crane from derailing.
- The end carriages have safety buffers to prevent damage if the crane runs into the end of the crane track or into another crane.
- The end carriages can be fitted with an additional derailing protection device on all four wheels (option).
- The end carriages can be fitted with guide rollers (option) to equalise the tolerances of the crane track. For this, one of the two end carriages is fitted with two horizontal guide rollers on both wheels. These run left and right close to the crane track. The crane is thus closely guided on one side. The other side has very wide wheels to balance out the tolerance.
The other end carriages (without guide rollers) can also be fitted with a derailing protection device on both wheels (option).
The end carriages of the sizes 280, 350 and 420:
- The end carriages of the sizes 280, 350 and 420 have a clamping piece on the powered wheel.
- The end carriages of the sizes 280, 350 and 420 have a special rigidity aid on the inside, called a clamp brace, which transfers the stress from the main girder to the end carriages.
The size 500 end carriages:
- The end carriages of size 500 are welded box girders with an optimised contour for high wheel loads.
- The size 500 end carriages are outstandingly robust and rigid.
Size 130-420 wheel blocks:
- The wheel blocks are fully automatically welded U-profiles with an installed trolley.
- The wheel blocks are attached to the main girder by a welded joint.
- The wheel blocks (according to the respective width of the crane track) have wheels with wheel flanges, which enable even running on the crane track and prevent the overhead travelling crane from derailing.
- The wheel blocks have safety buffers to prevent damage if the crane runs into the end of the crane track or into another crane.
- The wheel blocks can be fitted with an additional derailing protection device on all four wheels (option).
- The wheel blocks can be fitted with guide rollers (option).
Disposing of the end carriage
If the end carriage is to be disposed of:
- Dismantle the end carriage to the extent possible.
- Observe local regulations concerning disposal and recycling.
- Dispose of the individual parts sorted by material in an environmentally sound manner.
- Plastic parts should be recycled with plastic waste.
- Remove brake linings and friction clutch linings and dispose of these multiple components as hazardous waste.
- Remove oil or grease from the crane travel drives and dispose of as a lubricant.
- Sort lines and plug-in connections by material and bring them to a recycling centre.
- Recycle steel structures as scrap metal.
- Dispose of electronic components as scrap electronic parts.
Installing and connecting
This section applies to anyone who works on the crane prior to its use
The end user of the crane is responsible for the proper qualifications of the commissioning personnel.
Examples of qualified persons:
- Persons with comprehensive knowledge from specialist training in engineering and in the electrical systems of cranes.
- Persons with sufficient experience in the operation, installation and maintenance of cranes.
- Persons with comprehensive knowledge regarding the relevant technical rules, directives and safety regulations applicable in the respective country.
- Persons receiving regular training from ABUS.
ABUS assumes no liability for damage due to incorrectly performed commissioning work done by unqualified personnel.
ABUS recommends having the commissioning work performed by the ABUS assembly team.
Installing the crane track
So that the overhead travelling crane travels steadily, smoothly and without great wear and tear, the crane track must be properly installed. Otherwise the overhead travelling crane will travel unsteadily and the wheels will wear out more rapidly.
The design and installation of the crane track must be taken into consideration upon construction of the building and planned together with the architects and structural engineers.
Observe the following points amongst others:
- The building supports and building beams or concrete supports or concrete girders as well as the brackets should be designed in such a way that the crane track can be welded onto them without difficulty.
- Only have welding work done by companies certified as per EN 1090 EXC-3.
- Monitor welded joints according to this standard.
- Design welded joints to at least quality class B of DIN EN ISO 5817.
- Clean the anchor plates (in the concrete brackets) or the steel brackets (to the building supports) prior to welding. They must be free of dirt, rust, scaling, paint, grease and oil.
- Cut the crane track joints at an angle of 45 degrees. Deburr the cut edges and clean. The gaps between the crane tracks should be as small as possible. The abutting crane track segments should not be misaligned laterally nor offset in height.
- For bolted crane tracks: firmly tighten all bolts with the correct tightening torque.
- Clean the crane tracks. They must be free of grease, oil, paint and dirt.
- Secure the crane track with suitable end stoppers.
- Provide the entire crane track with appropriate corrosion protection (e.g. paint)
Installation overview
The following sections show how the end carriage is installed.
- First, the safety buffers are installed on the ground. See “Installing the safety buffers”.
- The the end carriages are bolted to the crane's main girder. See “Welding on the wheel block”.
- Damage to paintwork is also repaired (see “Repairing damage to paintwork”).
- As a final step the screws of the end carriages are tightened with the correct tightening torque. See “Fastening the end carriages tightly”.
Welding on the wheel block
The chamfered edges on the wheel block can be attached to the larger crane construction using a weld seam.
When welding the wheel blocks, the following points must also be observed:
- Only have welding work done by companies certified as per EN 1090 EXC-3.
- Monitor welded joints according to this standard.
- Design welded joints to at least quality class B of DIN EN ISO 5817.
- Set out filler material for S355 structural steel according to the joint faces.
- Clean the appropriate joint faces before welding.
The must have a purity of SA 2 ½ according DIN EN ISO 12944 and be free of dirt, rust, scaling, paint, grease and oil.
Installing the safety buffers
In case the safety buffers are not installed:
Buffer plate
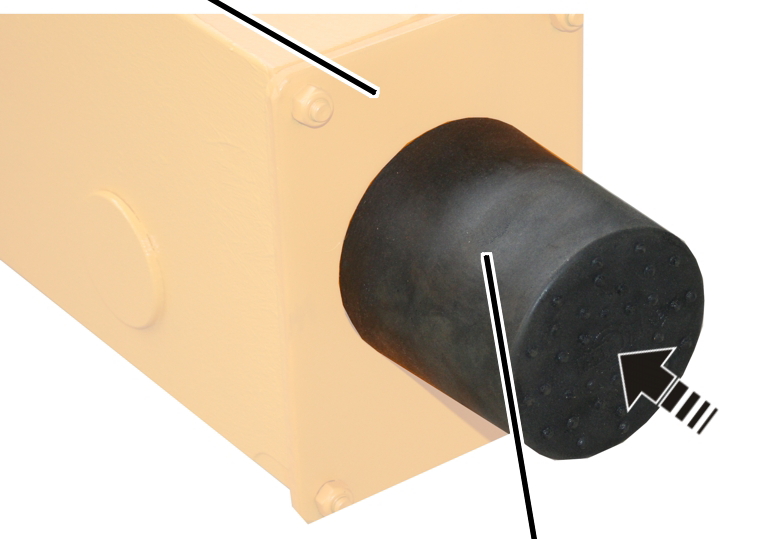
- Screw safety buffers (4x) into the buffer plates. Approx. 30 Nm.
The safety buffer must be in contact with the buffer plate and there must be no gap between them, otherwise the impact will be absorbed by the screw and not by the safety buffer.
Bolting on the end carriage
Assigning the end carriages
Letter position markers
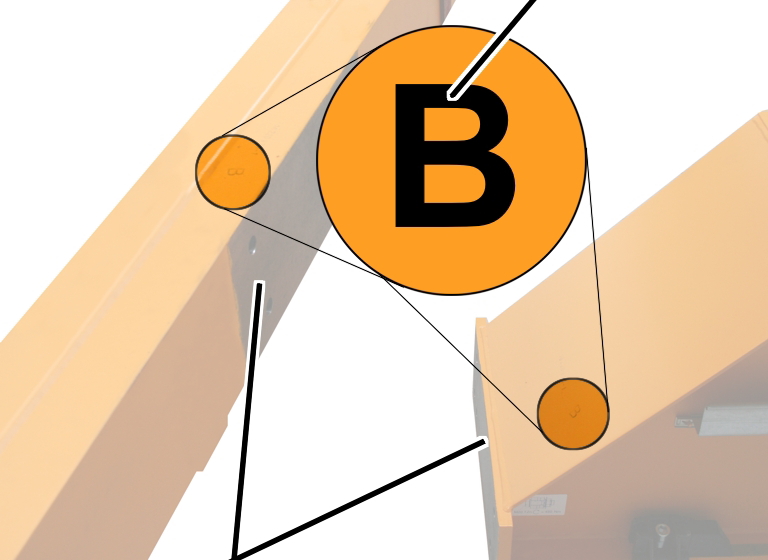
- Look for the letter position markers A and B (for the installation sequence) on the main girders and end carriages.
- Lay both end carriages on the joint faces of the main girder in such a way that the letter position markers match.
Preparing the bolt connection
Residual paint
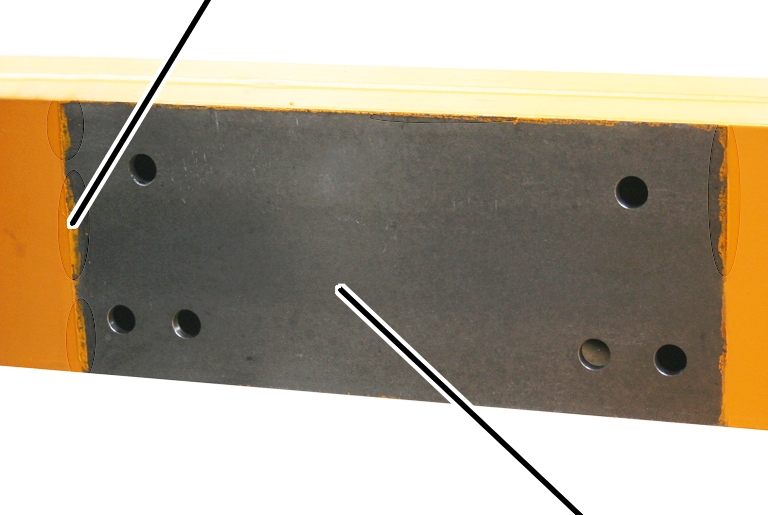
- Thoroughly clean the joint faces on the entire surface.
There should not be any rust, dirt, paint or similar impurities on them.
- Lift the end carriages in front of the main girders. The hole patterns must lie exactly over one another.
Checking the high-tensile bolts
- Check the high-tensile bolts. The high-tensile bolts must meet these requirements:
Material |
Size |
Lubrication |
|
|---|---|---|---|
High-tensile bolt (hexagonal) |
10.9 |
M20 |
|
Washer |
C 45 |
HV 21 |
MoS2 |
High-tensile nut (hexagonal) |
10 |
M20 |
MoS2 |
- The high-tensile bolts and mounting plate with high-tensile nuts may only be installed with tightening torque a maximum of twice. If they are installed more than twice with tightening torque, the high-tensile bolts as well as the mounting plates with the high-tensile nuts must be scrapped.
Should it be necessary to loosen the high-tensile bolts during installation, the same high-tensile bolts can be reused a maximum of once more, otherwise the lubrication will no longer be sufficient!
- The high-tensile nuts and washers must be galvanised and lubricated with MoS2.
- High-tensile bolts which have been installed on a crane for a lengthier period may not be used again.
The end carriages are initially only installed by manually screwing until hand-tight. They are finally firmly screwed (with a tightening torque) only after the crane is on the crane track and the trolley and all other components are installed. By doing so, the main girders can settle and the crane is not warped on the crane track. See “Fastening the end carriages tightly”.
Bolting on the end carriage
Clamp brace
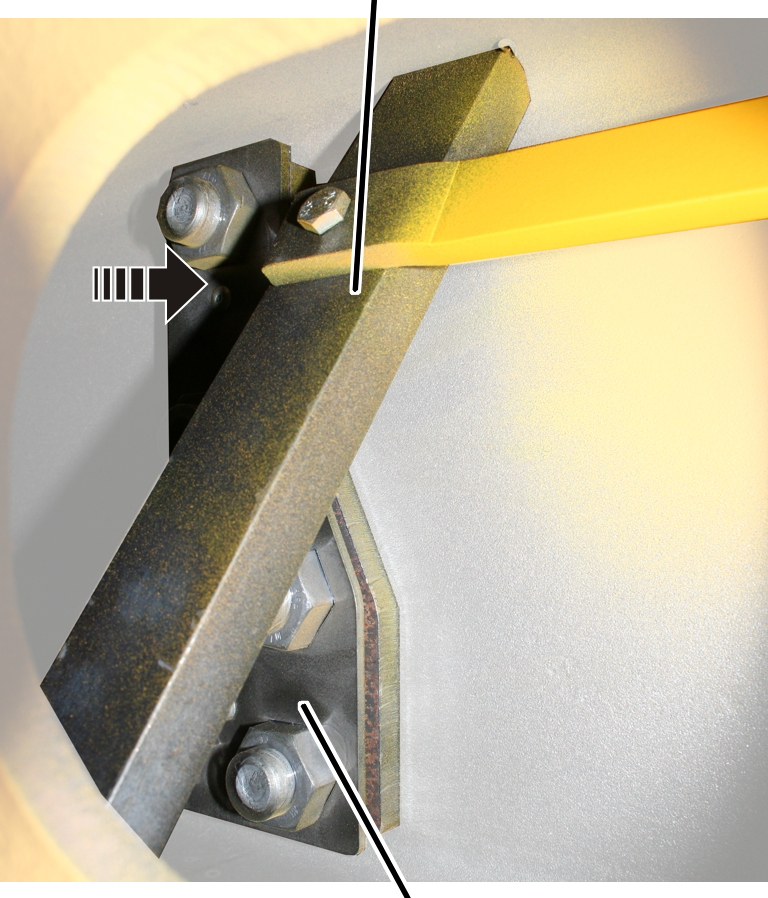
- Only with end carriages of size 280, 350 and 420: Do not move, dismantle or damage the clamp brace in the end carriage.
- Place the mounting plate in the end carriage and hold it so the hole pattern properly overlaps.
High-tensile bolt
with washer
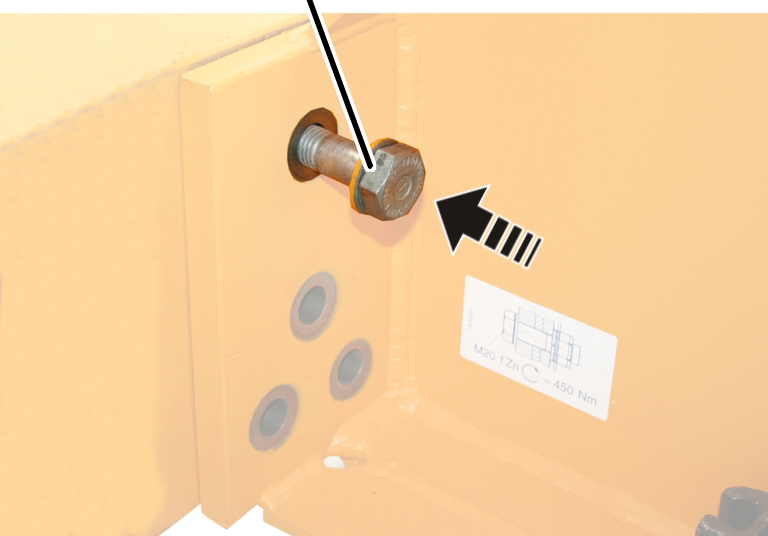
- Place the washers on the high-tensile bolts with the bevel (chamfered edge) to the head of the screw.
- Insert the high-tensile bolts and washers from the outside into the screw holes and screw on so they are somewhat loose.
- Screw on the second end carriage following the same sequence of steps.
Sealing the access portal
Access portal
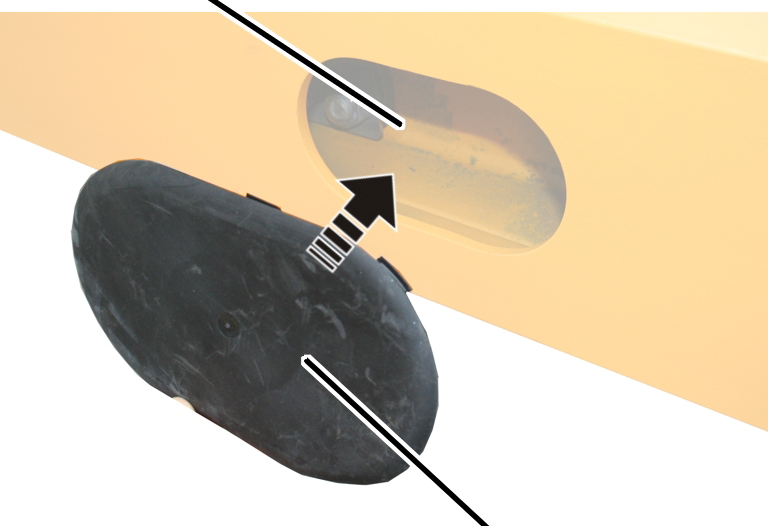
- Seal the access portal with a cap.
Only for rainwater or condensation water
This work step only applies if the crane comes into contact with rainwater or condensation water (e.g. outdoor operation, semi-exposed building etc.)
Sealing the joint faces
The gap between the two joint faces must be sealed so that no water can penetrate and rust the metal parts.
Joint
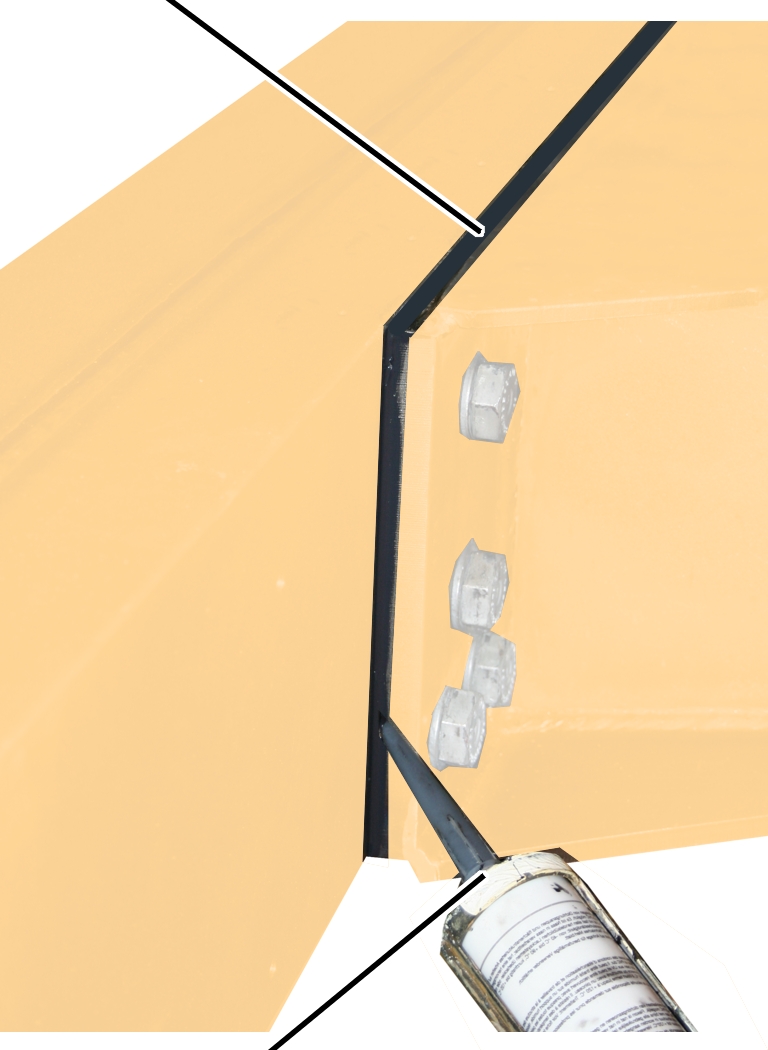
- Squeeze sealant (supplied) with a cartridge applicator gun into the joints between the main girders and the end carriages. Only left, right and above.
The joints below remain free so that entrapped water can drain off.
- Smooth the sealant in the joint.
- Clean away any smeared sealant.
- If necessary, reapply the sealant. The sealant can be handled “wet on wet”, no drying time is necessary.
Repairing damage to paintwork
- Repair damage to paintwork caused during transportation and installation.
Fastening the end carriages tightly
Once all components have been installed, the entire crane has settled as a result of the weight, and the stress is relieved. For this reason, the end carriages can only now be tightened with the tightening torque.
Central high-tensile bolt
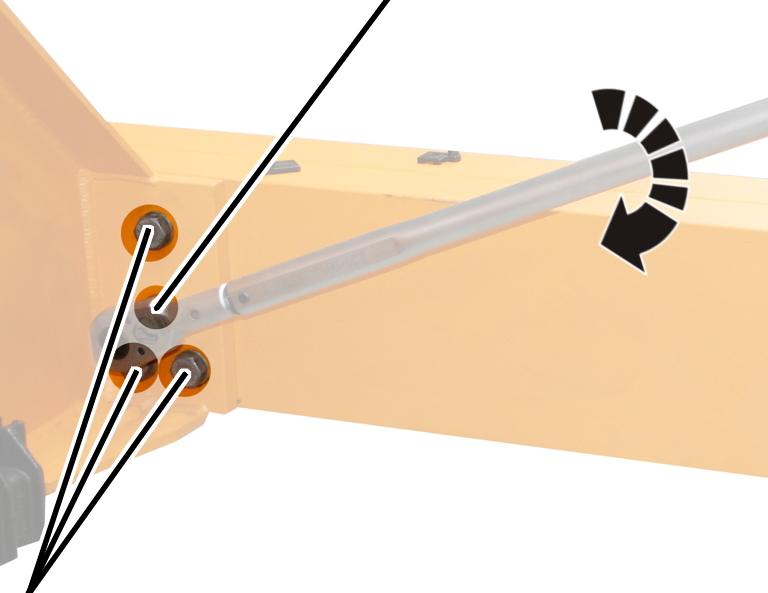
high-tensile
bolts
- Only tighten high-tensile bolts with the appropriate torque wrench.
- Do not use an impact wrench.
- Do not tighten high-tensile bolts using turn-of-nut tightening.
- Tighten the central high-tensile bolts on both sides (left and right on the end carriage). Use a torque wrench to 300 Nm.
- Next, tighten the remaining high-tensile bolts, alternating between left and right. Use a torque wrench to 300 Nm.
- Then tighten all high-tensile bolts in the same sequence. Use a torque wrench to 450 Nm.
Note
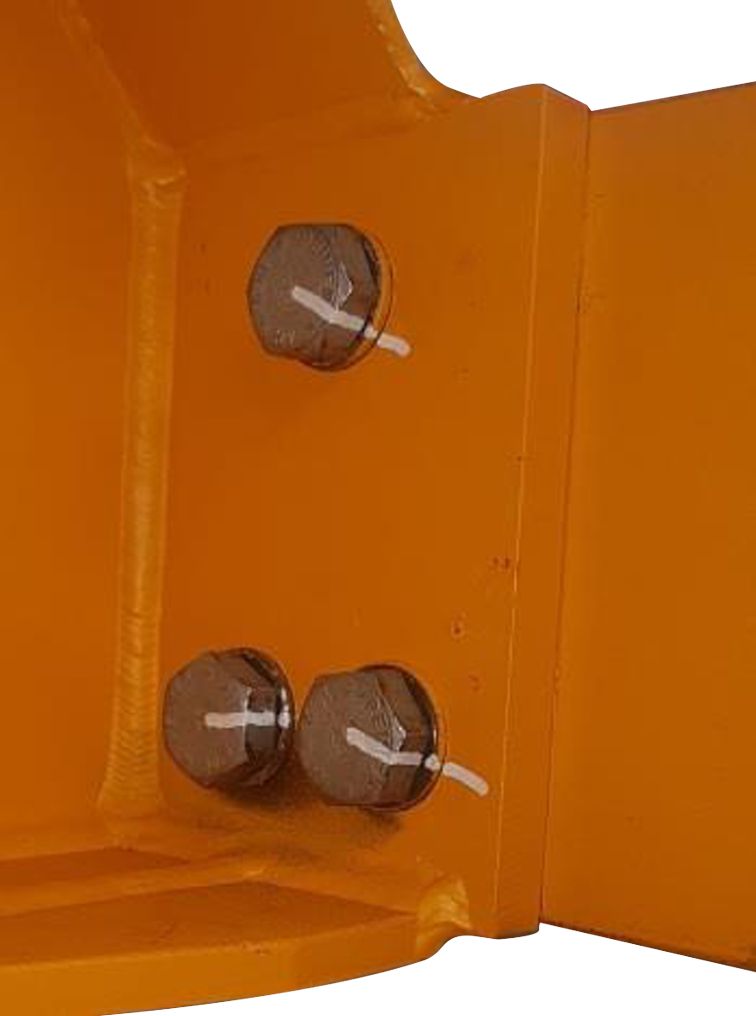
Mark the high-tensile bolts with a permanent marker with a continuous line from the bolt head over the washer to the plate. This serves as proof that all high-tensile bolts have been tightened with tightening torque.
Inspection
This section applies to anyone who inspects and accepts the crane in accordance with occupational health and safety requirements
The end carriages must be regularly inspected in order to guarantee safe operation. The end user is responsible for these regular inspections.
At the start
Test intervals
The regular inspection is performed at least once annually.
Under certain conditions, more frequent regular inspections may be necessary. Reasons include:
- Frequent operation at the load capacity
- Working in multiple shifts
- Frequent use
- Dusty or chemically aggressive environment
The end user is responsible for checking the requirements and determining the test intervals. ABUS will gladly assist you if questions arise.
Requirements for the examiner
The end user of the crane is responsible for the proper qualifications of the examiner.
Examples of qualified persons:
Persons with comprehensive knowledge from specialist training in engineering and in the electrical systems of cranes.
- Persons with sufficient experience in the operation, installation and maintenance of cranes.
- Persons with comprehensive knowledge regarding the relevant technical rules, directives and safety regulations applicable in the respective country.
- Persons receiving regular training from ABUS.
Scope of the test
The qualified person inspecting the crane is responsible for the type and scope of the test.
Overview: Inspecting the crane
In addition to the points described here, all points outlined in the other supplied product manuals must also be checked.
The decision as to whether the crane is in perfect condition may be made only by the person inspecting the crane. Any inadequacies, if found, must be eliminated. The examiner decides whether the crane has to be tested again afterward.
If locally applicable regulations specify further tests, these are likewise to be carried out.
Additionally, at least the following points must be checked:
- Check the wheel flange for wear. See “Inspecting the wheel flange wear”.
- Only for braking function or shut-down: check the braking distance of the end carriage in the limit switch range. See “Checking the braking distance”.
- Check the wear on the guide rollers. See “Checking the wear on the guide rollers”.
- Check the diameter of the wheels. See “Checking the diameter of the wheels”.
- Check the condition of the safety buffer. See “Inspecting the condition of the safety buffer”.
Inspecting the wheel flange wear
Only for wheels with a wheel flange
The undercuts in the wheel flanges are a sign of wear on the wheel flange.
Wheel flange
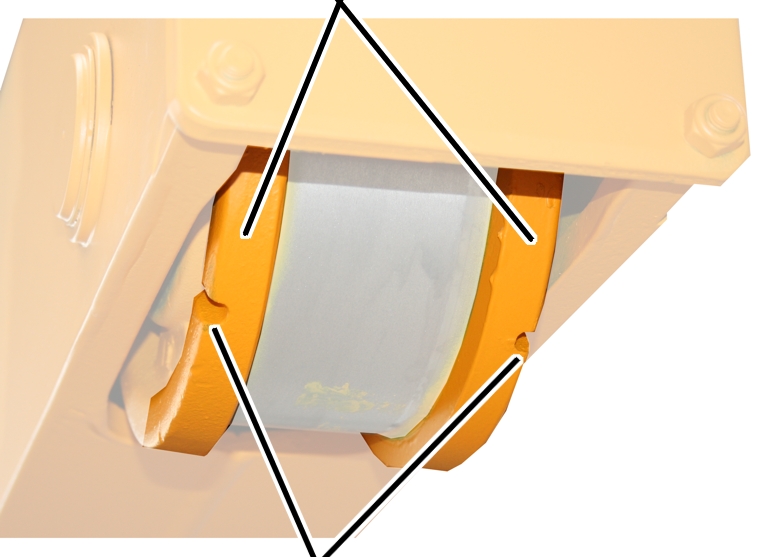
- Inspect the wheel flanges of the wheels: The wheel flanges must not be worn so much that a continuous crack can be seen in the wheel flange (rather than undercuts). If they are, replace the wheels.
Checking the braking distance
Only for braking function or shut-down
The brake on the crane travel drives is worn during operation. This lengthens the braking distance of the crane. The crane may therefore strike the end stopper of the crane track too fast and put excess pressure on the supporting structure (e.g. the building).
- Suspend a load on the load hook which corresponds to the maximum load capacity of the crane.
- Move the crane into the limit switch range.
- Check the braking distance:
For braking function: the crane must run only at low speed just in front of the end stopper.
For shut-down: the crane must come to a standstill just in front of the end stopper.
- If the braking distance is too long: Adjust the brake on the crane travel drive. See the product manual for the crane travel drive.
Checking the wear on the guide rollers
Only for four-roller guide rollers
This working step is only applicable if the guide roller unit is made up of four guide rollers per end carriage side.
The guide rollers must be clamped tight first in order to check wear.
Clamping the brackets tight
Turnable bracket
for guide rollersBracket on
the end carriage
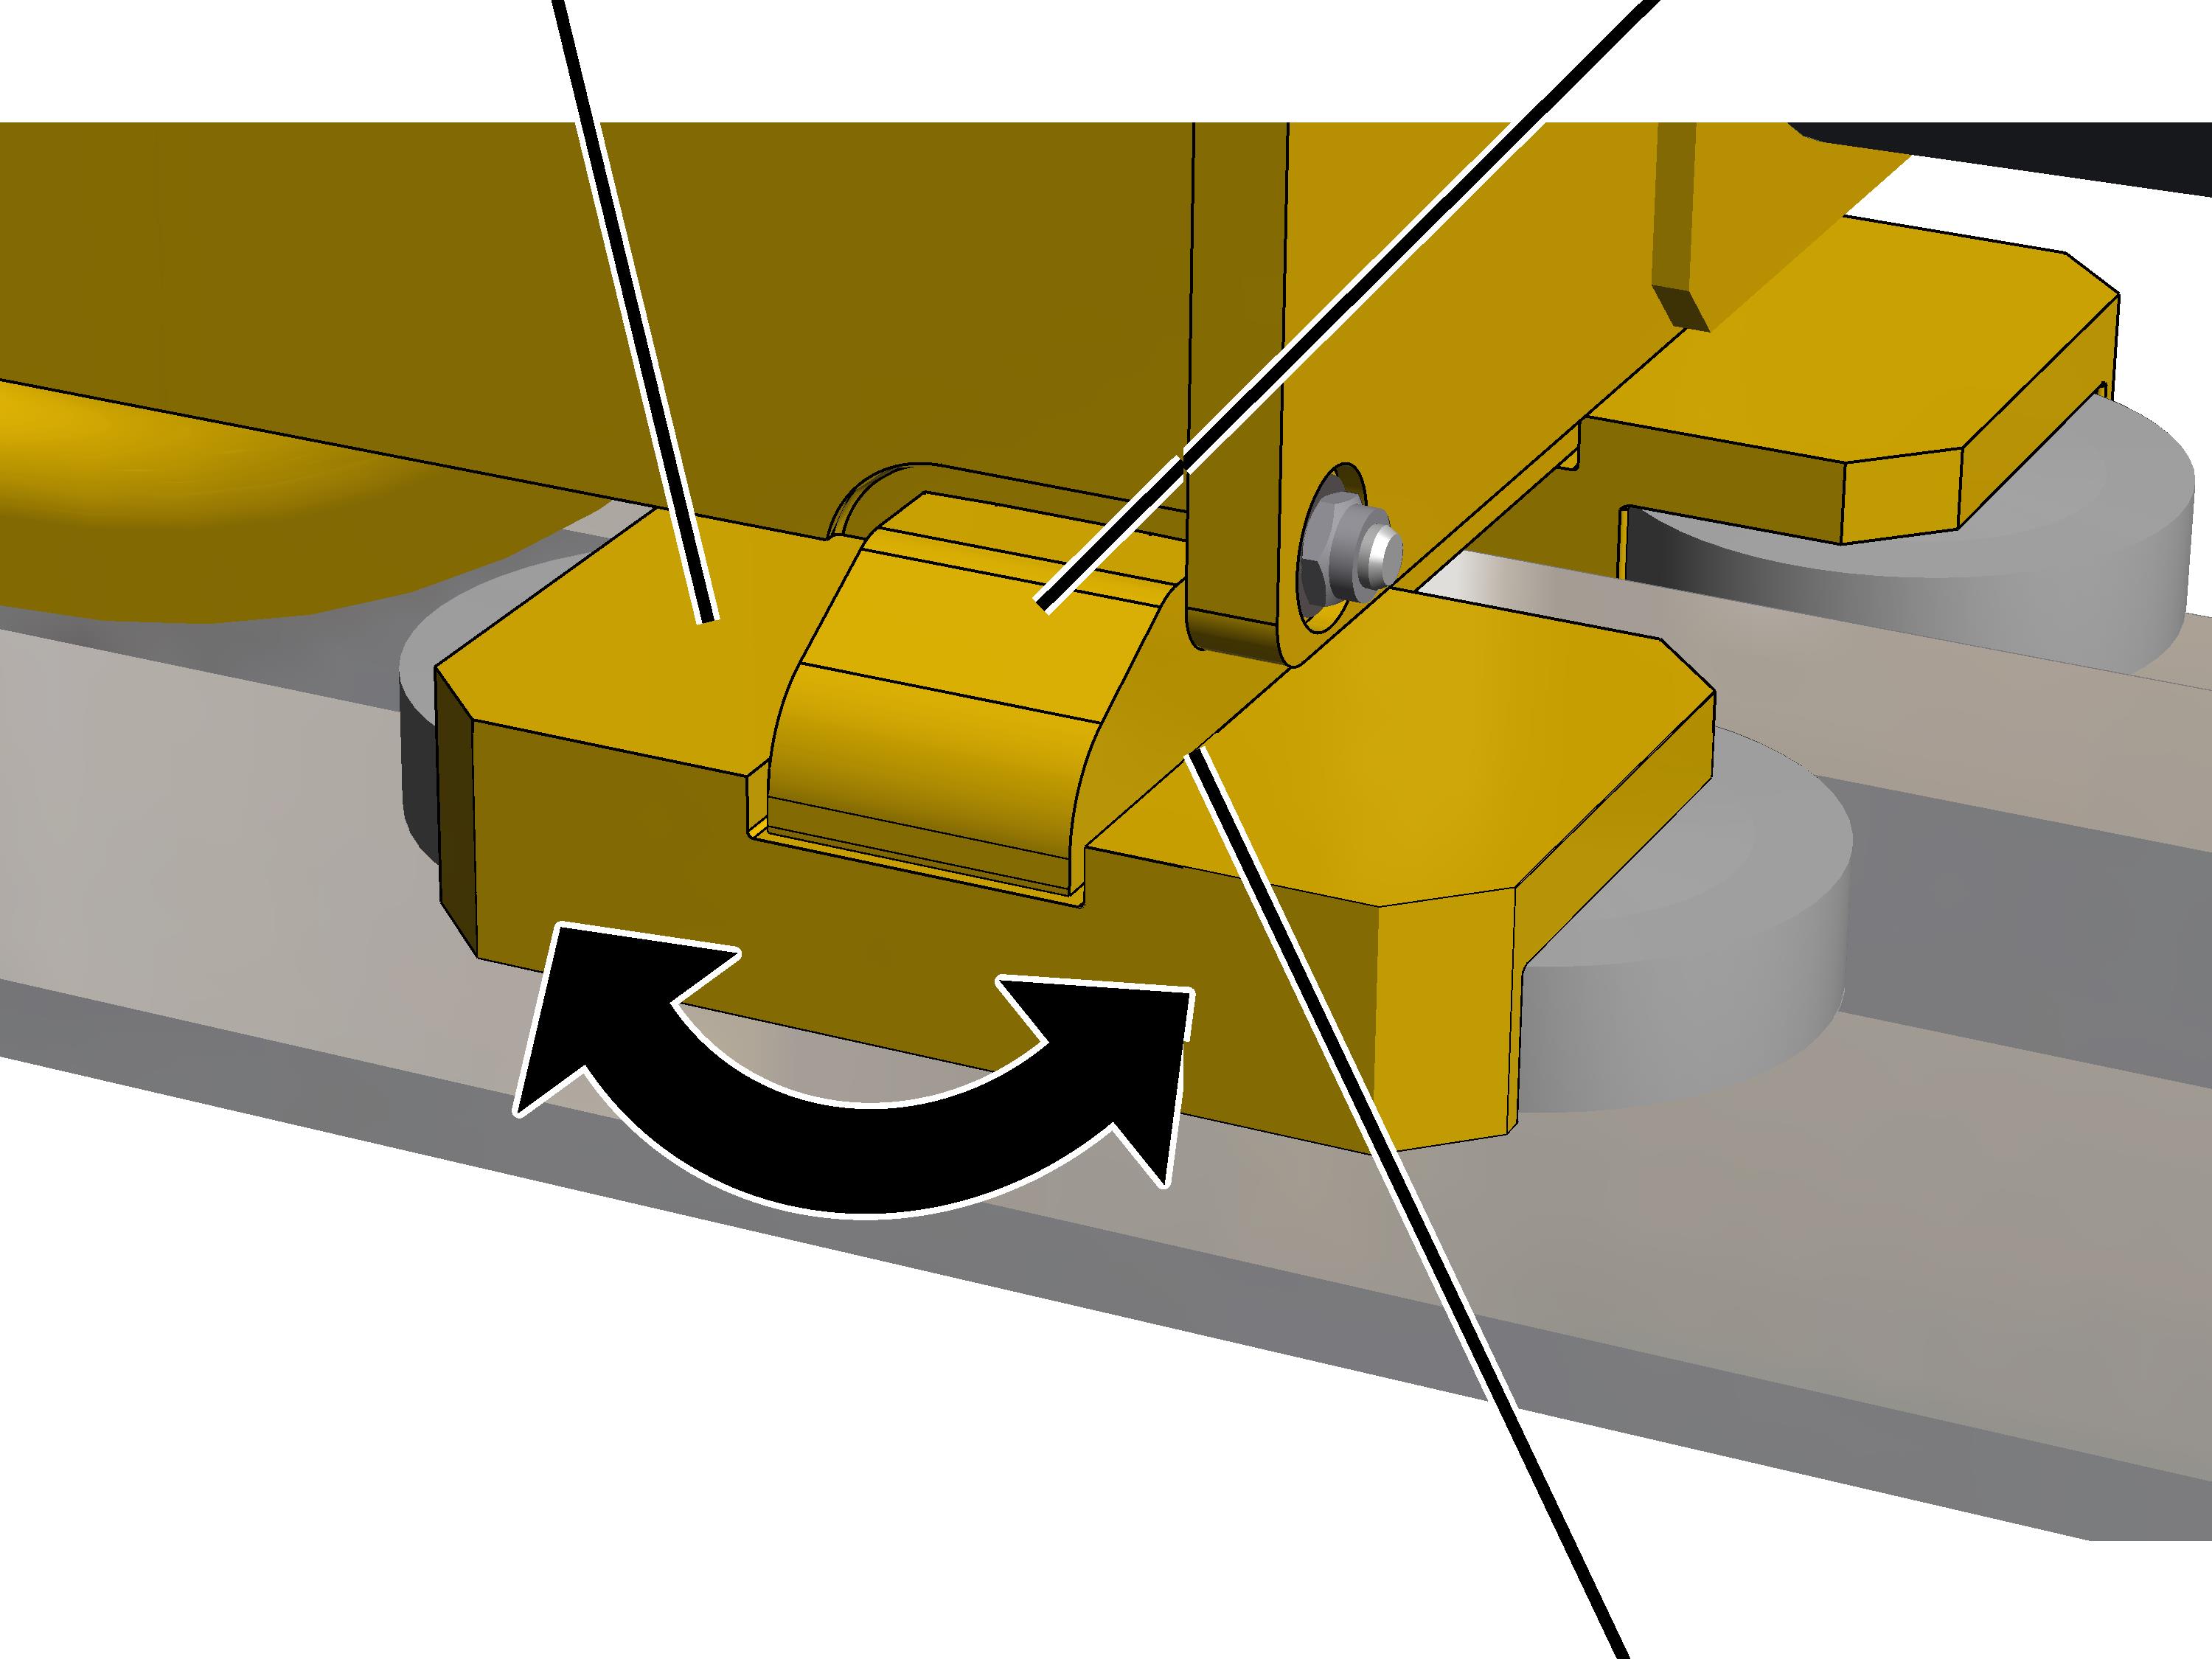
- Rotate the turnable bracket in such a way that it is parallel to the crane track.
- Insert a wedge in the gap between the bracket on the end carriage and the turnable bracket in order to clamp the guide roller unit tight.
- The turnable bracket can now no longer be displaced.
- Now measure the distance between the front and rear pairs of rollers and the crane track as described below.
Only for guide rollers
The wear on the guide rollers is checked based on the clearance between the guide rollers and the crane track.
Checking the wear
Guide roller
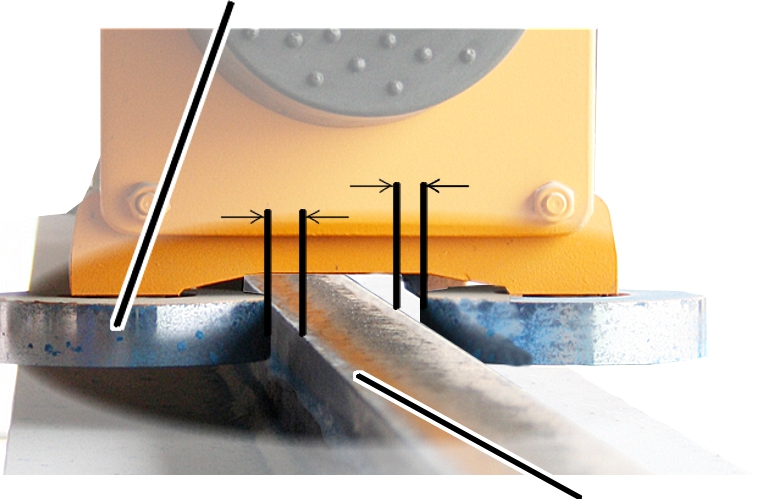
- Measure the distance between guide roller and crane track on both sides.
- The distance (between guide roller and crane track) on both sides together may not be greater than that specified in the table.
If the distance is greater than this, the guide rollers must be replaced.
Size (wheel diameter) |
Max. distance (total) to the crane track on both sides. |
Distance (total) on both sides with new guide rollers |
|---|---|---|
130 |
11 mm |
5 mm |
160 |
11 mm |
5 mm |
200 |
11 mm |
5 mm |
280 |
11 mm |
5 mm |
350 |
14 mm |
5 mm |
420 |
14 mm |
5 mm |
500 |
14 mm |
5 mm |
Determining the diameter for new guide rollers
If the distance between guide roller and crane track is too large (see previous section), the guide rollers must be replaced.
During operation of the crane, however, both the guide rollers and the crane track are subjected to wear. Since only the guide rollers can be replaced, they may need to be exchanged for larger ones than were previously used in order to compensate for the wear on the crane track.
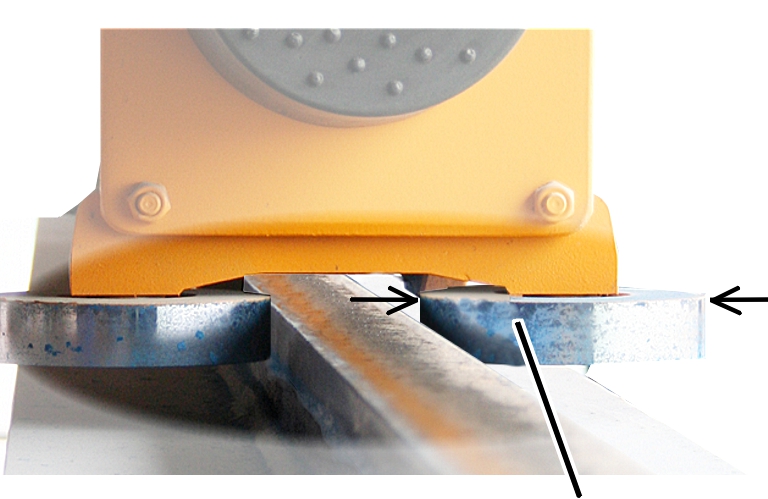
- If possible: Measure the diameter of the guide roller above the crane track.
This area of the guide roller frequently has no contact with the crane track and can therefore be used to determine the original diameter.
- Determine the diameter of the new guide roller:
- The distance between the guide rollers and the crane track should be as close possible to 5 mm (see also previous table). This applies to the entire length of the crane track.
- The distance between the guide rollers and the crane track may not be smaller than 5 mm. This applies to the entire length of the crane track.
Checking the diameter of the wheels
The running surfaces of the wheels become worn during operation. This reduces the diameter of the wheels.
Exposing the wheel
Buffer plate
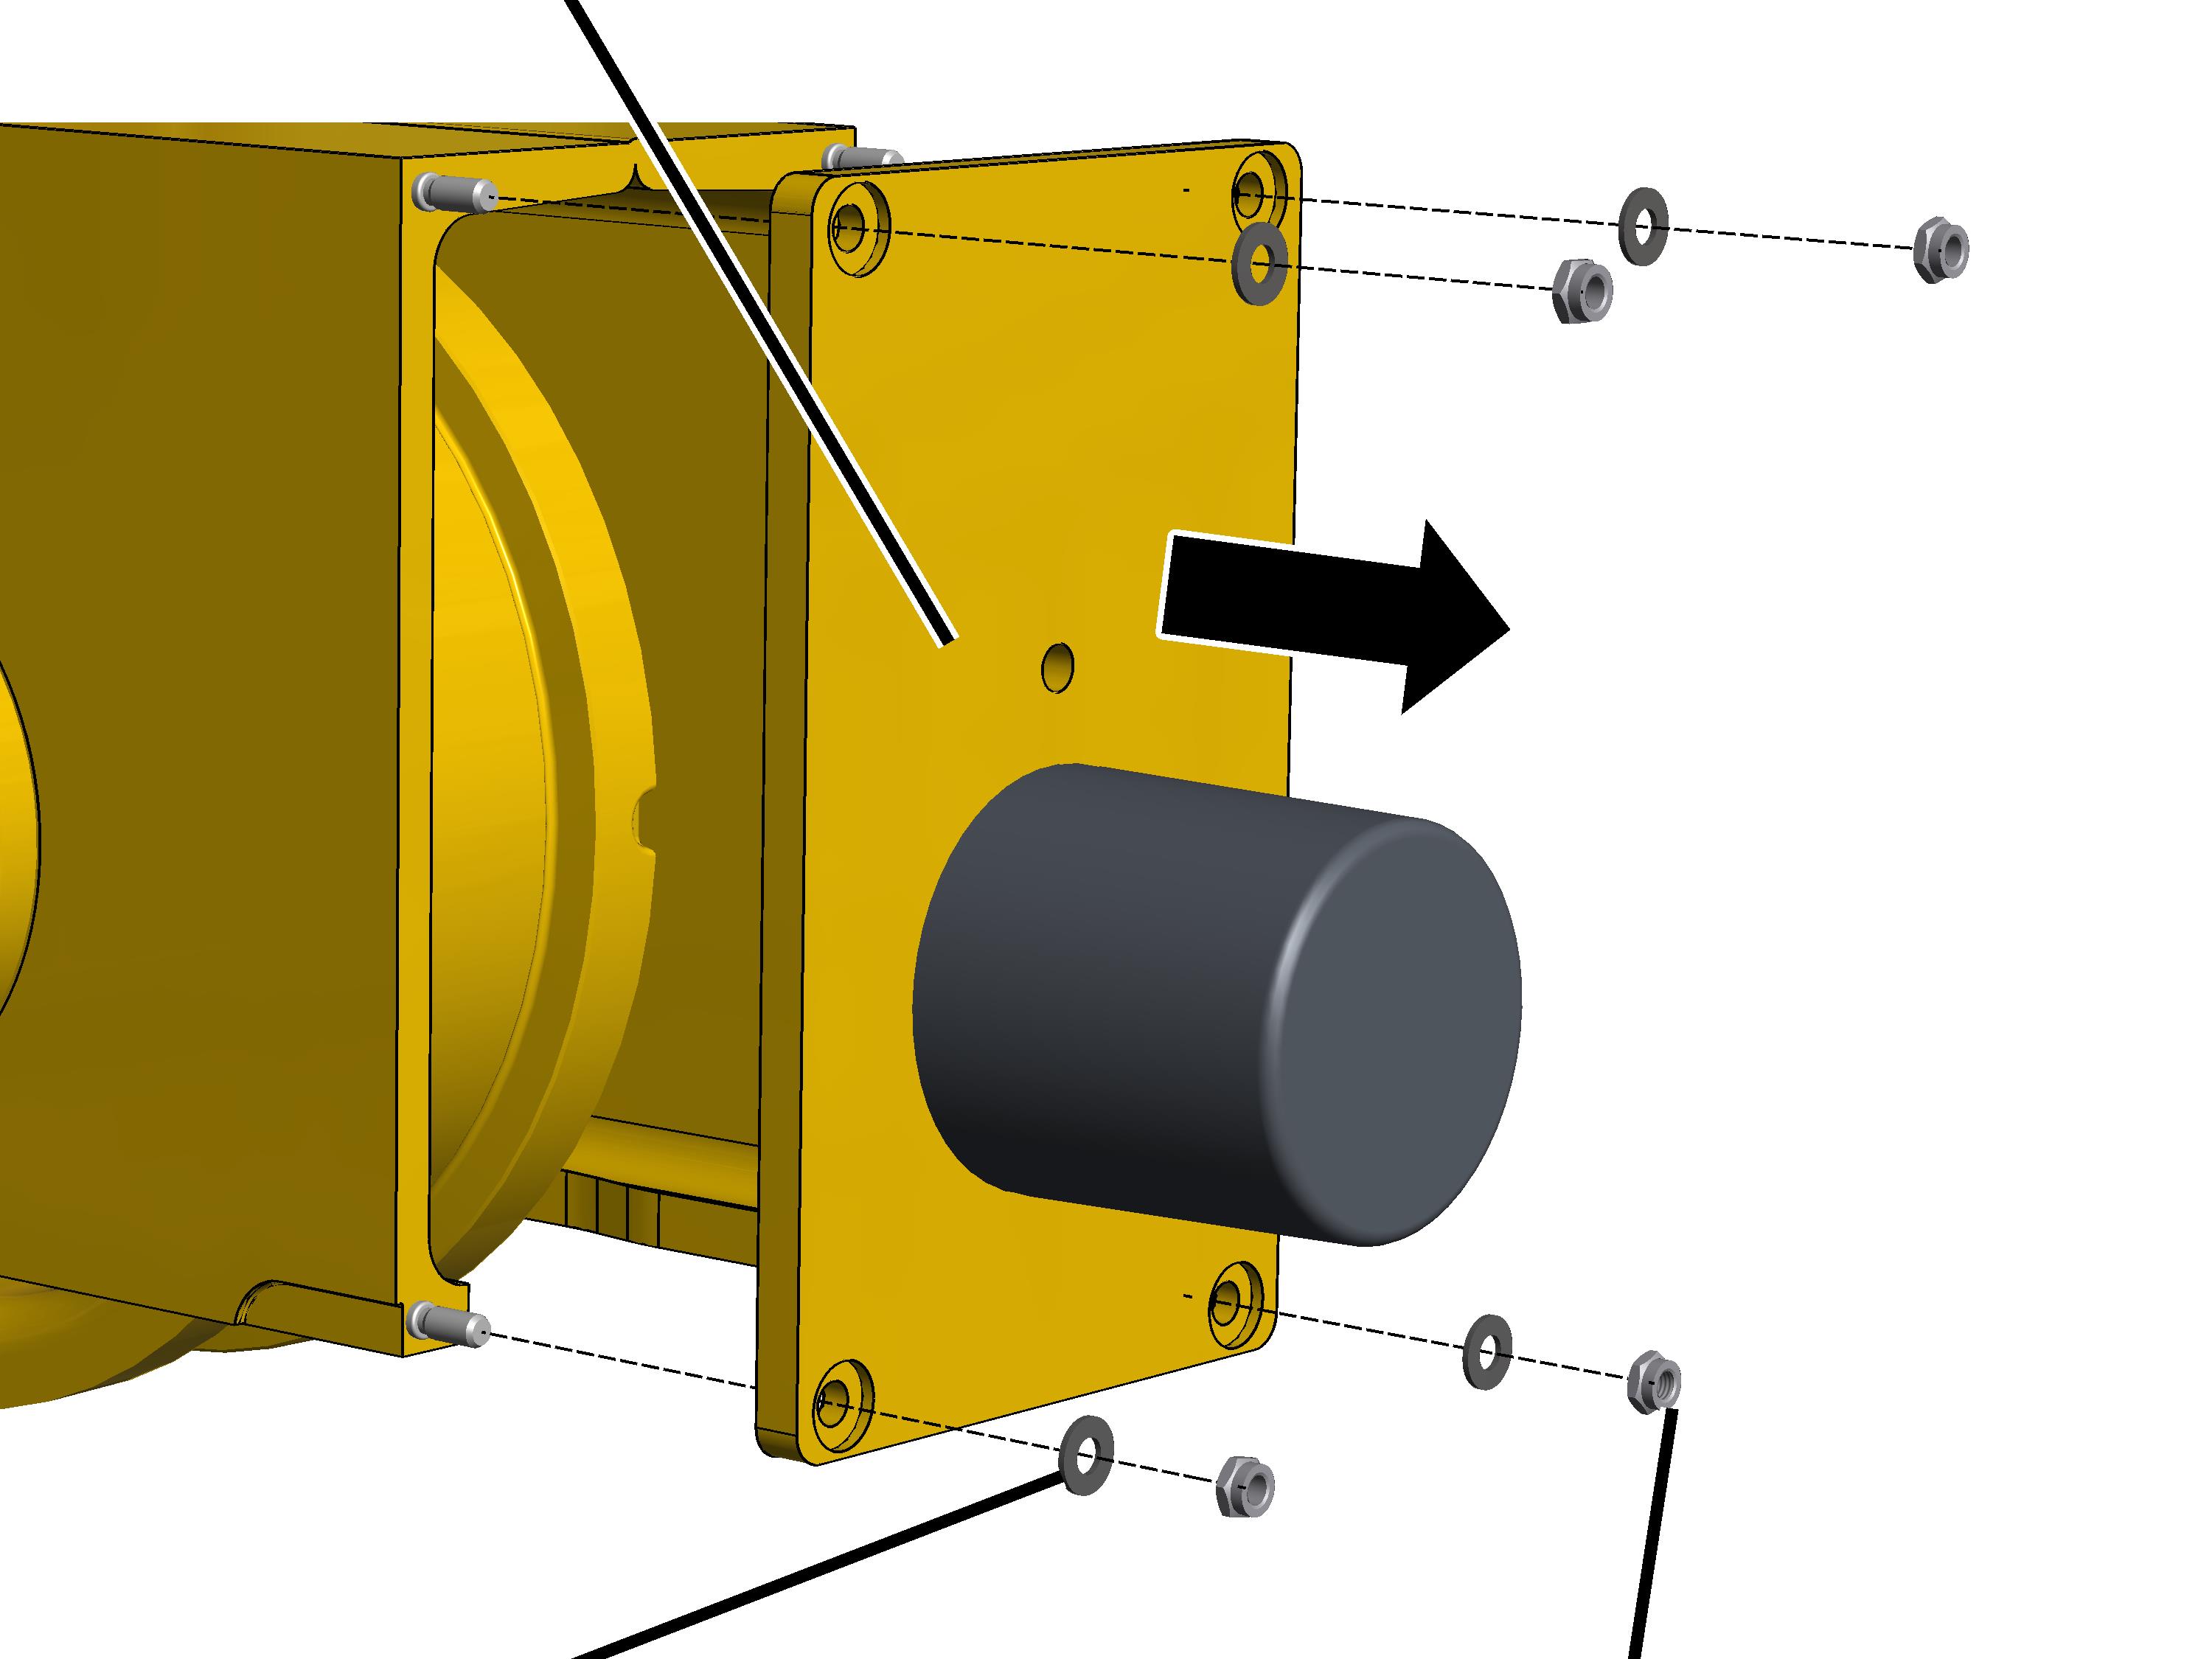
- Unscrew the self-locking nuts (4x).
- From size 160: remove the plastic washers (4x).
- Remove the buffer plate.
Measuring the diameter
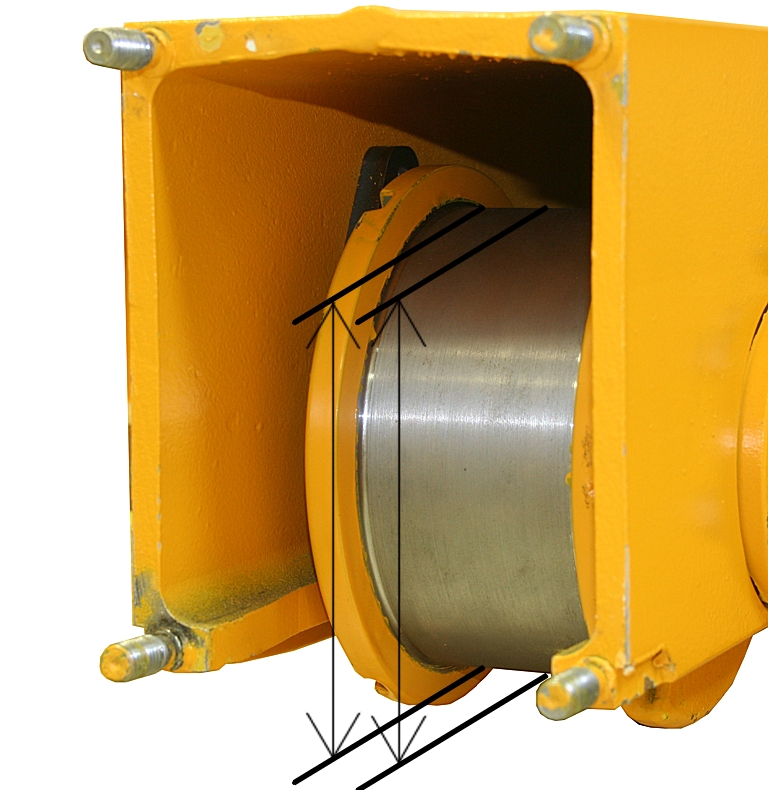
- Measure the diameter of the wheel at multiple points over the width of the wheel.
- The diameter may not be smaller than is specified in the table.
If the diameter is smaller, the wheel must be replaced.
Size |
Maximum permissible wear |
Minimum diameter of wheel |
|---|---|---|
130 |
-3 mm |
127 mm |
160 |
-3 mm |
157 mm |
200 |
-4 mm |
196 mm |
280 |
-5 mm |
275 mm |
350 |
-5 mm |
345 mm |
420 |
-5 mm |
415 mm |
500 |
-5 mm |
495 mm |
Measuring the difference in diameter
In addition, the driven wheels of the crane must be of uniform diameter so that the crane runs evenly on the crane track.
This means that the permissible deviation in the diameter of (opposite-lying) power-driven wheels is limited.
Only for a 4-wheel crane travel drive and 8-wheel cranes: the diameter does not need to be as similar as possible between all power-driven wheels, but only between the respective opposite-lying wheels of the crane.
- Determine the difference in diameter of the (opposite-lying) power-driven wheels.
The difference in diameter may not be larger than is specified in the table.
If the respective diameters of the wheels deviate from each other by more than this, the wheels must be replaced.
Size |
In the case of cranes subject to a lower workload (use in accordance with S2 or B3) |
In the case of cranes subject to a high workload (use in accordance with S3 or B4) |
|---|---|---|
130 |
2 mm |
1 mm |
160 |
2 mm |
1 mm |
200 |
2 mm |
1 mm |
280 |
3 mm |
1.5 mm |
350 |
3 mm |
1.5 mm |
420 |
3 mm |
1.5 mm |
500 |
3 mm |
1.5 mm |
Inspecting the condition of the safety buffer
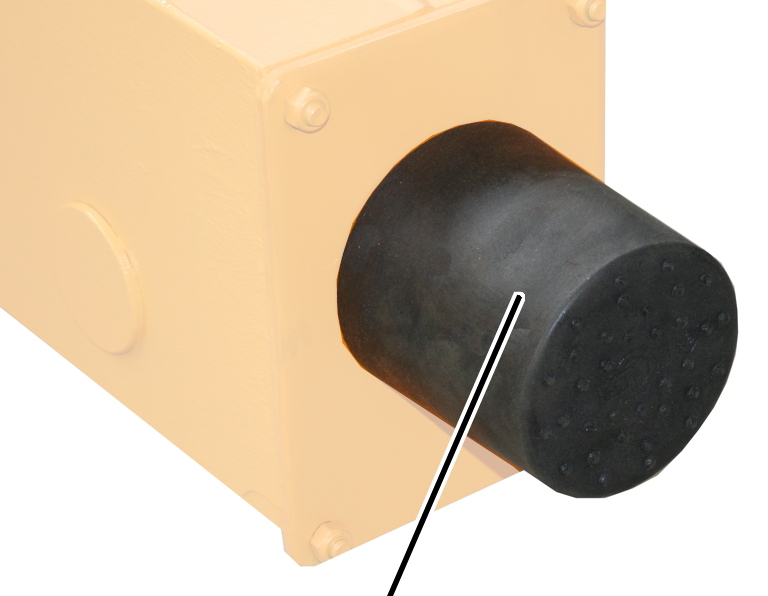
- Check all the safety buffers. The safety buffers must not be porous, pinched, bent or otherwise damaged.
- Check the material of the safety buffers all the way round. The plastic must not be cracked anywhere on the surface.
- Press the safety buffers with your finger. The safety buffers must be able to be pressed in slightly and be formable.
- If any of the safety buffers is damaged in any way whatsoever, replace all the safety buffers on the crane.
- If any of the safety puffers cannot be pressed in, replace all the safety buffers on the crane.
Maintenance
This section applies to anyone who maintains, repairs or modifies the crane.
The end user of the crane is responsible for the selection and proper qualifications of the maintenance personnel.
Examples of qualified persons:
- Persons with comprehensive knowledge from specialist training in engineering and in the electrical systems of cranes.
- Persons with sufficient experience in the operation, installation and maintenance of cranes.
- Persons with comprehensive knowledge regarding the relevant technical rules, directives and safety regulations applicable in the respective country.
- Persons receiving regular training from ABUS.
ABUS assumes no liability for damage due to incorrectly performed maintenance work done by unqualified personnel.
ABUS recommends having the maintenance work performed by ABUS Service.
Use only original ABUS replacement parts. Otherwise, all warranty claims will be rendered invalid.
Instructions regarding safety when performing maintenance work
Please follow the following safety instructions during all repair work on the crane:
- Switch off the mains switch. Secure the switch to ensure it cannot be turned back on accidentally.
- Unplug the mains disconnector plug from the socket on the crane panel. Secure the socket with a padlock to ensure it is not plugged back in accidentally.
- Use suitable lifting platforms and fall protection equipment.
- Adequately cordon off the operating range around the lifting platform.
- Switch off any other cranes using the same crane track or cranes working above or below the crane undergoing maintenance. Secure the switches to ensure they cannot be turned back on accidentally. Otherwise, other cranes could overturn the hoisting platform or crash into the crane undergoing maintenance.
- Notify personnel in the area that maintenance work will be performed.
- Only trained electricians should work on the crane electrical system!
- Even after the emergency stop button has been pressed, life-threatening high voltages are still present in the panels.
Disassembling the powered wheel
If the wheel is damaged or worn, it must be replaced by a new wheel.
The figures show the disassembly of a size 130 wheel. The removal of larger wheels does not essentially differ from this.
Preparing the crane
- Comply with occupational health and safety requirements.
- Prop up the end carriage close to the wheel.
Disassembling the crane travel drive
CouplingConnector housing
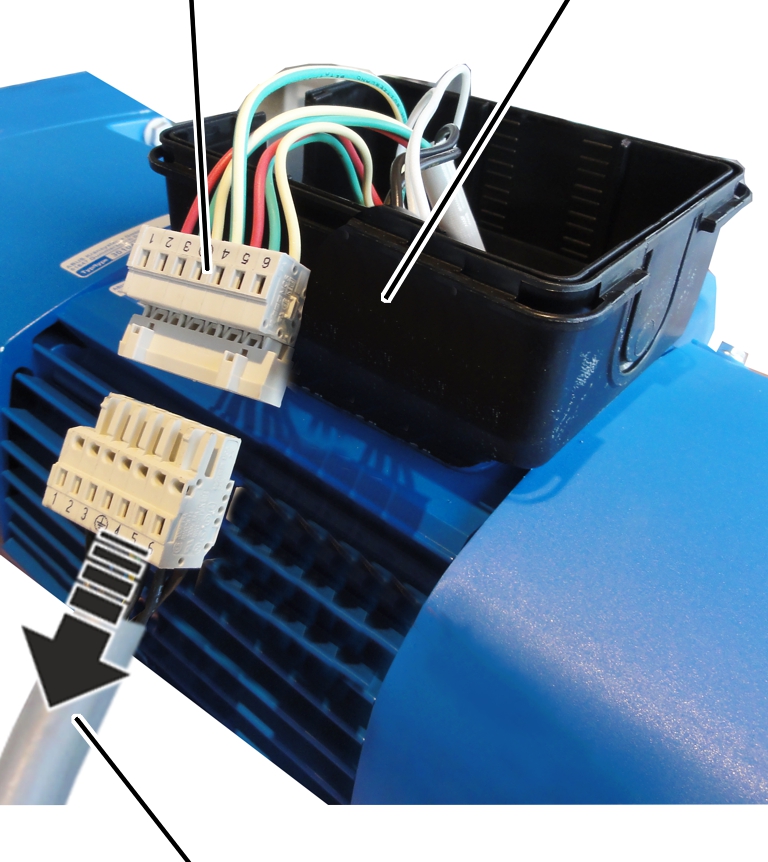
- Open the connector housing to the drive.
- Disconnect the connection cable from the coupler plug.
- Determine the weight of the drive. See the ABUS Drive product manual.
- Secure the drive so that the weight can be held safely and the output shaft will not be subject to load (e.g. insert in round sling).
Rib screws
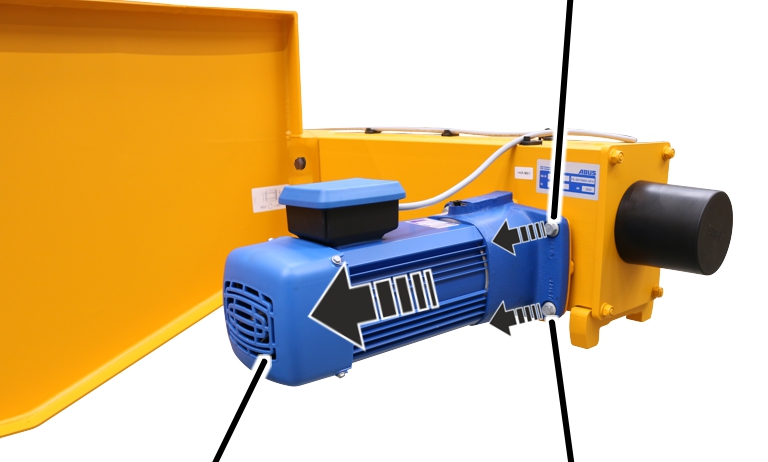
- Unscrew the rib screws (4x).
- Pull out the crane travel drive.
Exposing the wheel
Only with size 130 to 420
This work step applies only to end carriages of the sizes 130 to 420.
Buffer plate
- Unscrew the self-locking nuts (4x).
- Remove the plastic washers (4x).
- Remove the buffer plate.
Only for guide rollers, derailing protection device or end carriages of the sizes 280, 350 and 420
This section only applies if the end carriage has guide rollers or a derailing protection device. This work step also applies to end carriages of the sizes 280, 350 and 420.
ScrewsClamping element
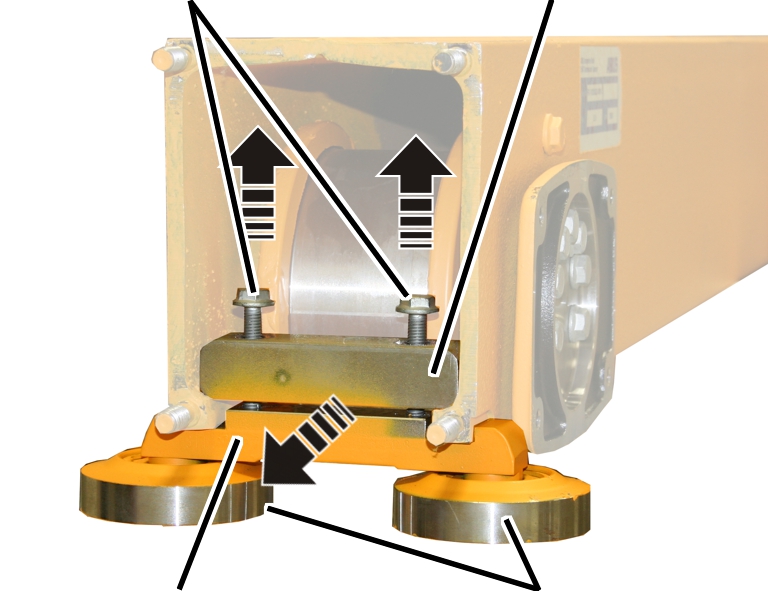
- Release screws (2x).
- Take out the bracket with guide rollers, derailing protection device or clamping piece.
Only for guide rollers on end carriages of size 500
This work step only applies if the size 500 end carriage has guide rollers.
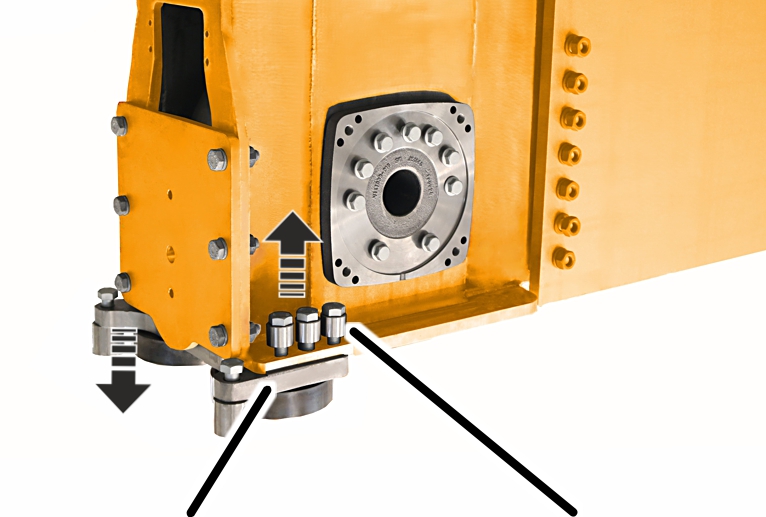
- Loosen high-tensile bolt M20x70 (3x) and remove bracket (1x) on both sides.
Only with size 500
This work step applies only to end carriages of size 500.
Mounting plateHigh-tensile nut M16
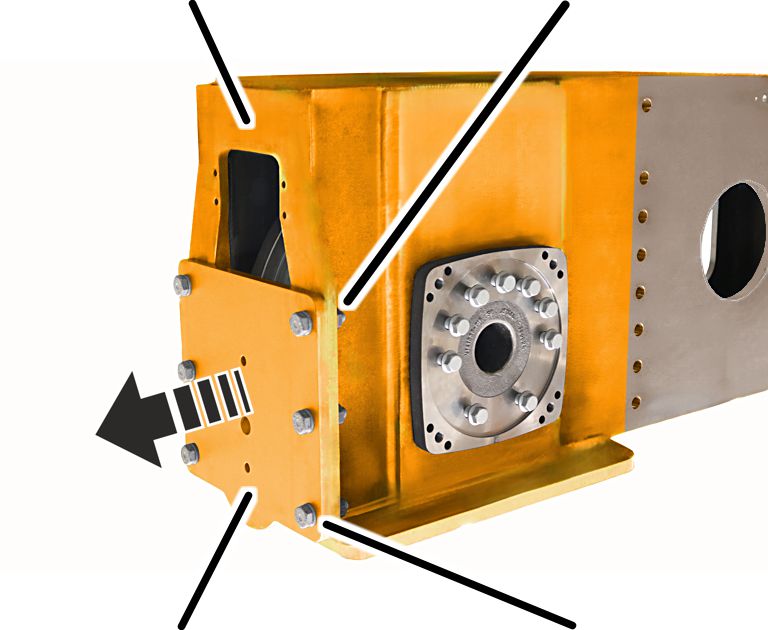
- Loosen high-tensile bolt M16x60 and remove the buffer plate from the mounting plate.
Removing the wheel
Retaining screw
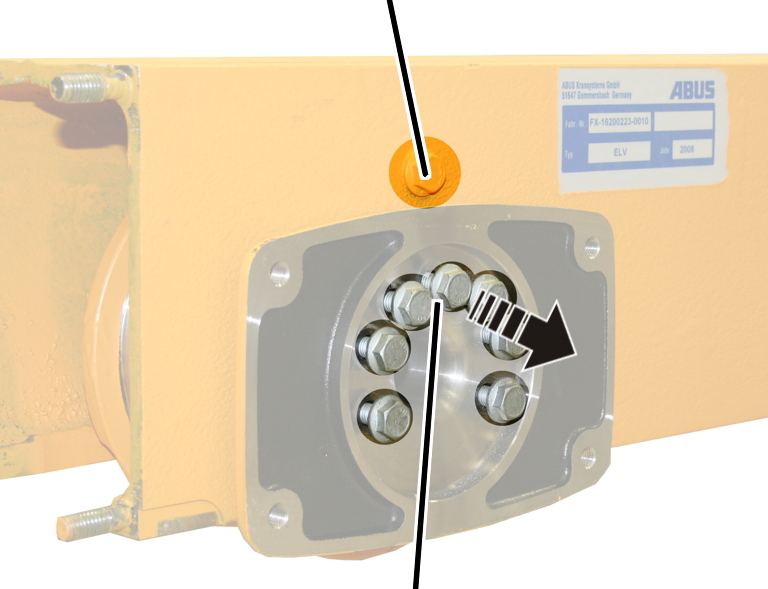
- Unscrew and remove all rib screws on the bearing flange. Do not unscrew and remove the retaining screw(s).
Retaining screw
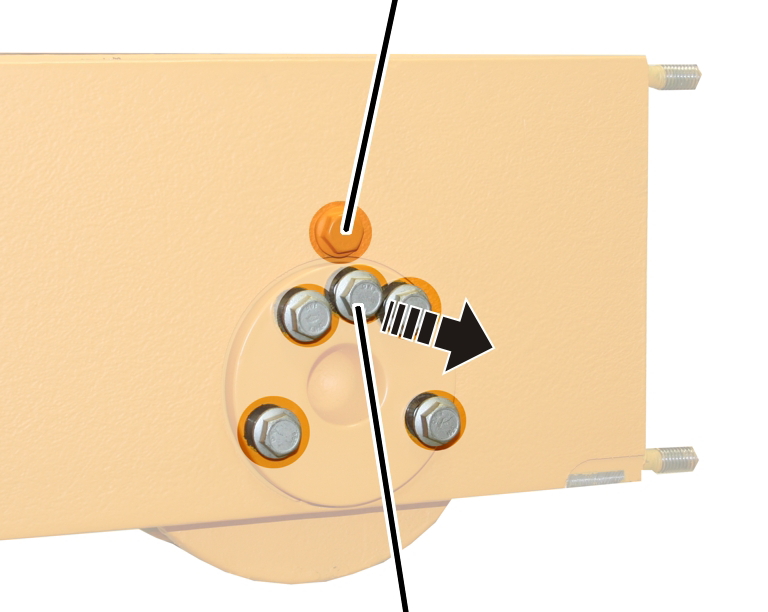
- Unscrew and remove all rib screws on the bearing bolt. Do not unscrew and remove the retaining screw(s).
Bearing boltBearing flange
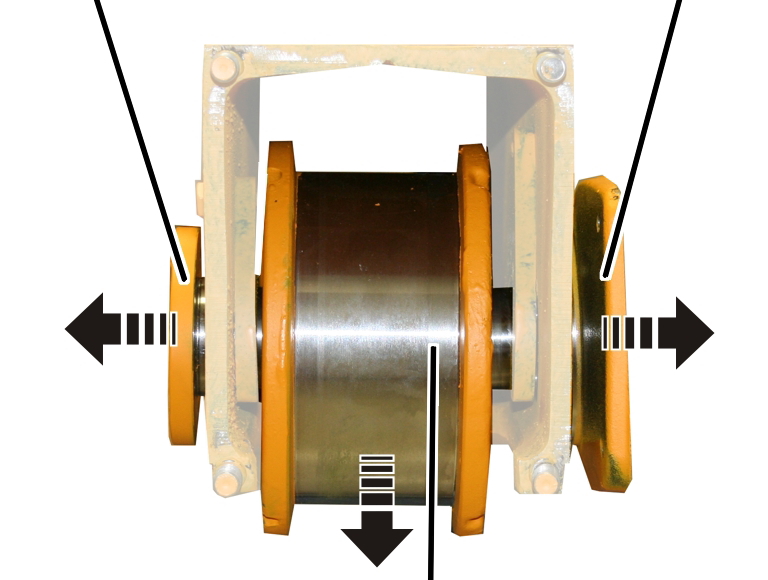
- Take out the bearing bolt, bearing flange and wheel.
Note:
Only for size 420 with crane travel drive 420 V: An adapter is also inserted on the bearing flange. If this cannot be easily taken off, it can remain on the bearing flange when the wheel is removed.
Tip:
To be able to easily remove the bearing flange from the end carriage, screw two or four screws in the corners of the bearing flange and thereby press the bearing flange off the end carriage.
Only with size 500
This work step applies only to end carriages of size 500.
Tip:
Threaded holes
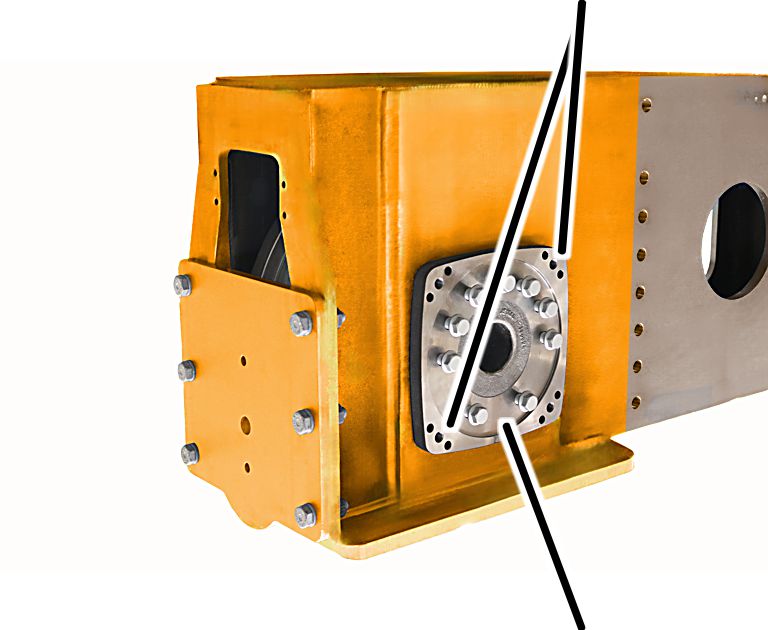
To be able to remove the bearing bolts more easily, insert two screws into free threaded holes on the bearing bolt, opposite each other. This makes it easy to push the bearing bolt out of the end carriage.
Installing the powered wheel
If the wheel is damaged or worn, it must be replaced by a new wheel.
The figures show the installation of a size 130 wheel. The installation of larger wheels does not differ significantly.
Fitting the wheel
Bearing
boltBearing
flange
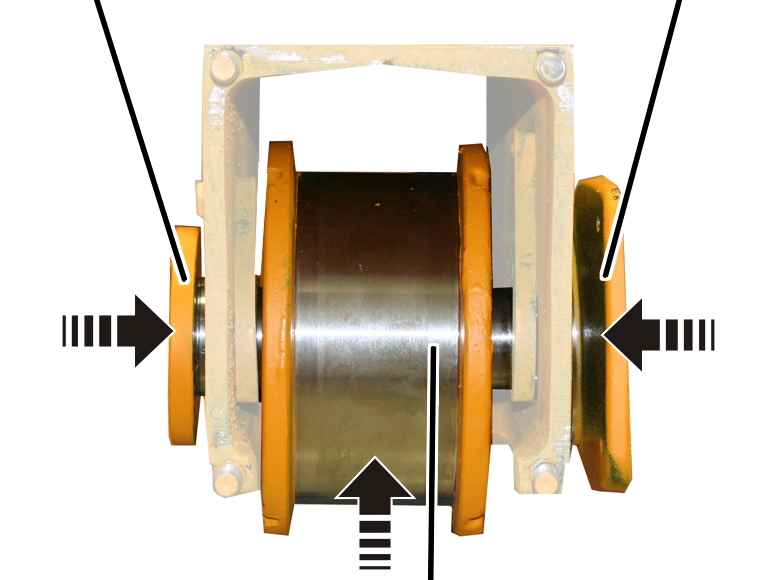
- Clamp the wheel in the end carriage. It does not matter which side faces inwards or outwards.
- Insert the bearing bolt and bearing flange. If necessary, lightly hammer the bearing bolt and bearing flange.
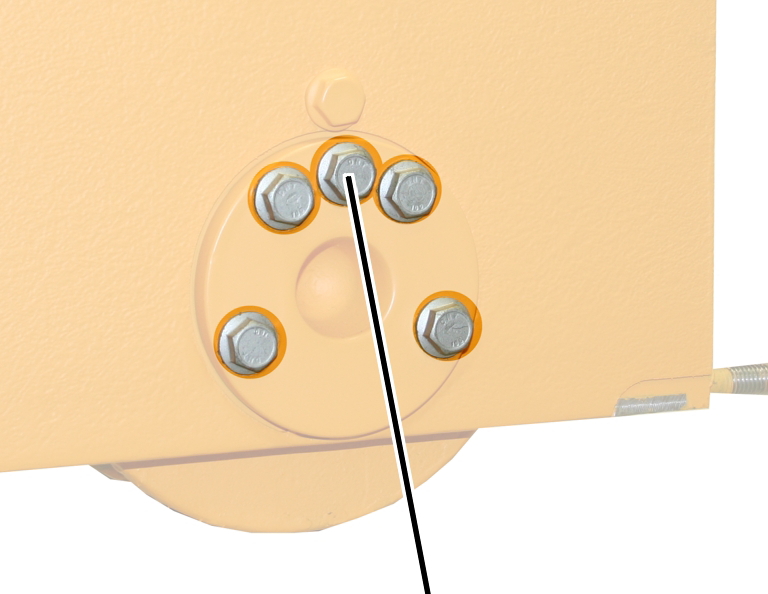
- Tighten the rib screws in stages.
Wheel Ø |
Strength category |
Number |
Screw |
Tightening torque |
|---|---|---|---|---|
130 |
10.9 |
5x |
M8x25 |
42 Nm |
160 |
10.9 |
5x |
M8x25 |
42 Nm |
200 |
10.9 |
5x |
M10x30 |
85 Nm |
280 |
10.9 |
5x |
M12x40 |
130 Nm |
350 |
10.9 |
8x |
M12x40 |
130 Nm |
420 |
10.9 |
8x |
M16x40 |
330 Nm |
500 |
10.9 |
5x |
M16x60 |
330 Nm |
Only for size 420 with crane travel drive 420 V
This work step only applies if an end carriage size 420 is to be installed with a crane travel drive size 420 V.
Mounting the adapter
Bearing flange
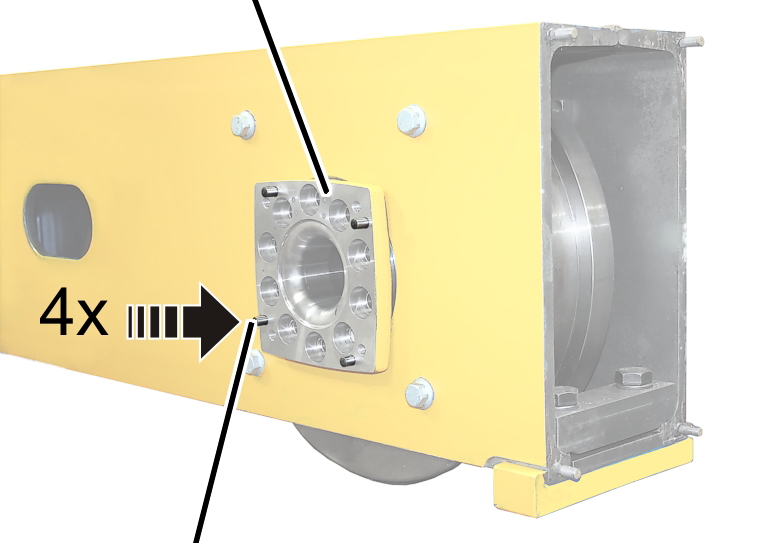
- If necessary: Insert the pins (4x) in the bearing flange.
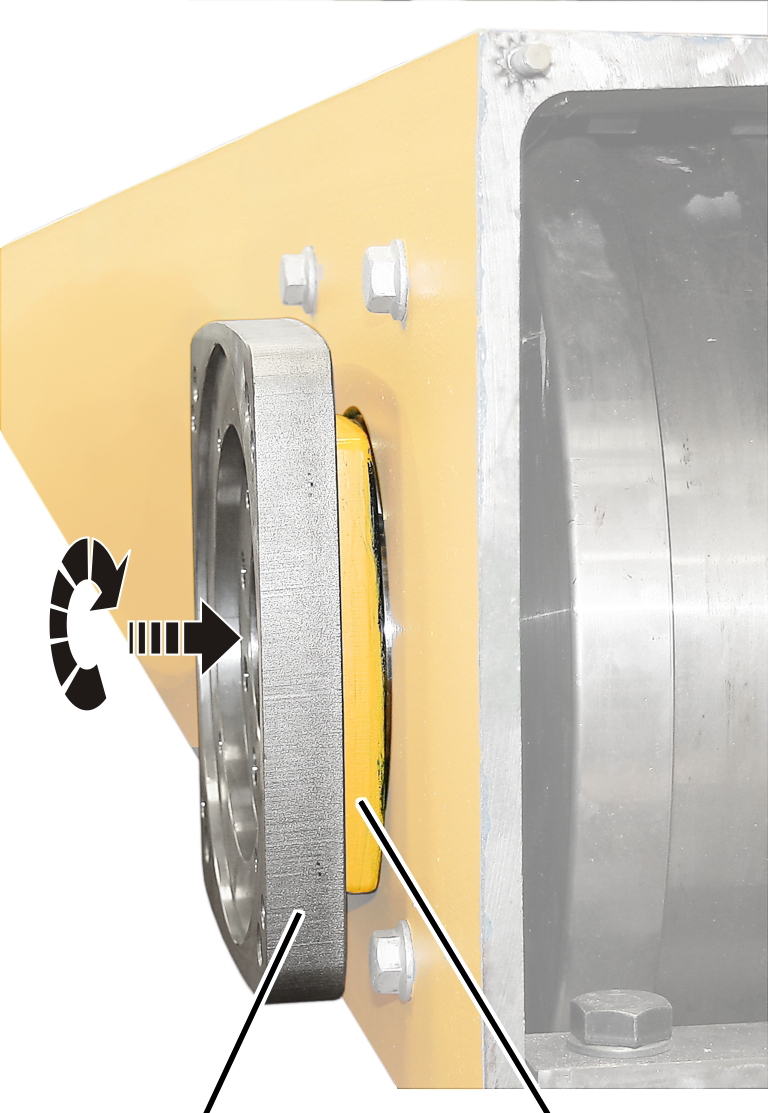
- Turn the adapter to match the hole pattern.
- Place the adapter on the pins on the bearing flange.
Rib screws
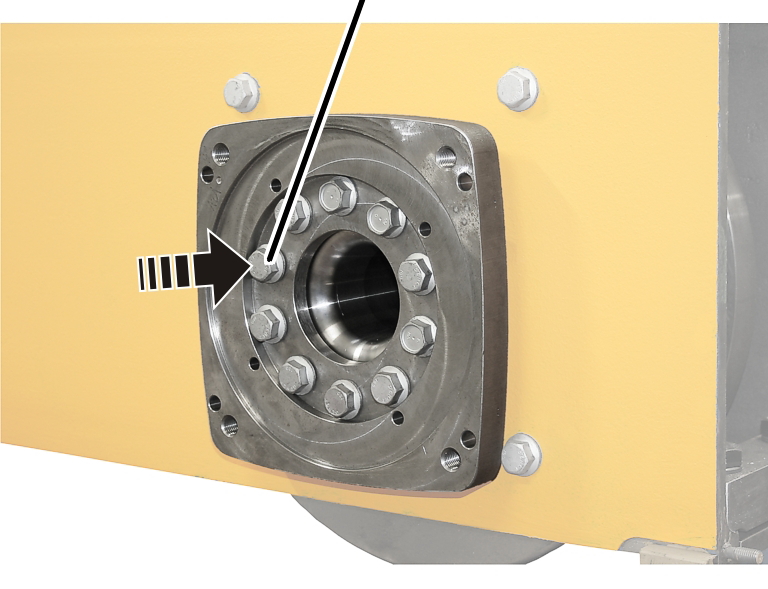
- Insert the rib screws M16x70 (10x) through the adapter and bearing flange.
Fastening the bearing flange
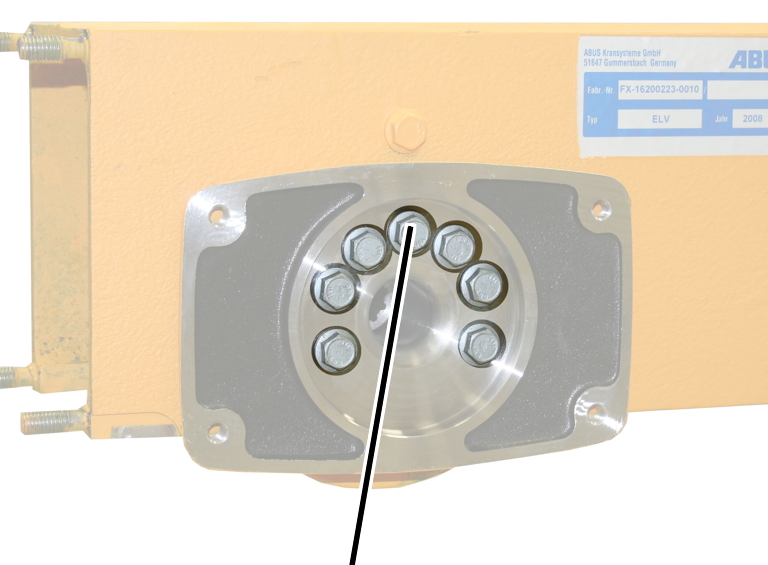
- Tighten the rib screws in stages.
Wheel Ø |
Strength category |
Number |
Type |
Tightening torque |
|---|---|---|---|---|
130 |
10.9 |
7x |
M8x25 |
42 Nm |
160 |
10.9 |
7x |
M8x25 |
42 Nm |
200 |
10.9 |
7x |
M10x30 |
85 Nm |
280 |
10.9 |
7x |
M12x40 |
130 |
350 |
10.9 |
10x |
M12x40 |
130 |
420 with crane travel drive 420 |
10.9 |
10x |
M16x40 |
330 |
420 with crane travel drive 420 V |
10.9 |
10x |
M16x70 |
330 |
500 |
10.9 |
9x |
M16x60 |
300 |
Assembling the end carriage
Only with end carriages of the sizes 280, 350 and 420
This work step applies only to end carriages of the sizes 280, 350 and 420.
ScrewsClamping element
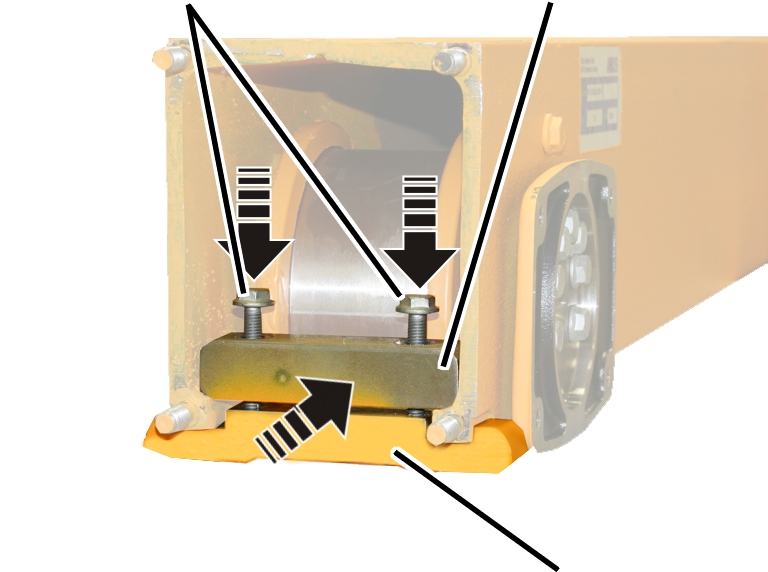
- Insert clamping piece.
- Tighten screws (2x).
Wheel Ø |
Type |
Kind |
Tightening torque |
|---|---|---|---|
130 |
M8x45 |
Rib screw |
42 Nm |
160 |
M10x50 |
Rib screw |
85 Nm |
200 |
M10x50 |
Rib screw |
85 Nm |
280 |
M12x60 |
Hexagon head screw |
130 Nm |
350 |
M20x75 |
Hexagon head screw |
300 Nm |
420 |
M20x75 |
Hexagon head screw |
300 Nm |
Only for guide rollers on end carriages of size 130 to 420
This work step only applies if the size 130 to 420 end carriage has guide rollers.
ScrewsClamping element
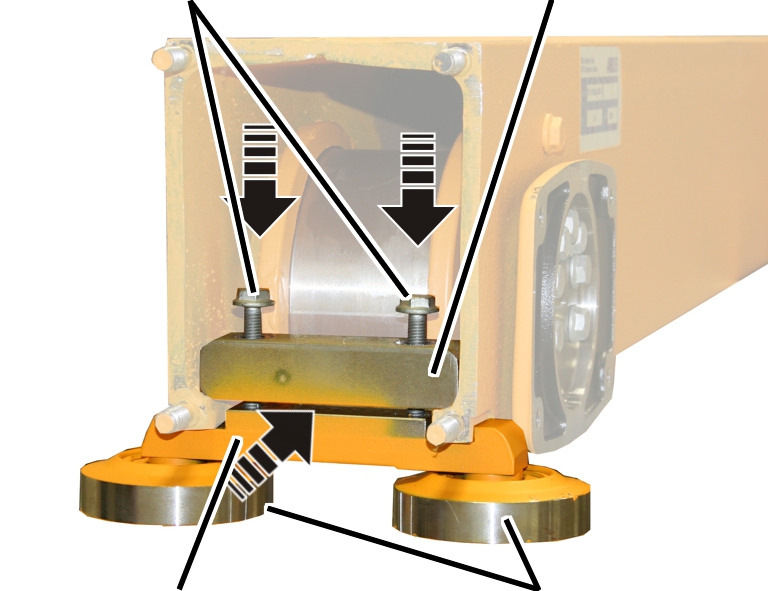
- Insert bracket with guide rollers.
- Tighten screws (2x).
Wheel Ø |
Type |
Kind |
Tightening torque |
|---|---|---|---|
130 |
M8x45 |
Rib screw |
42 Nm |
160 |
M10x50 |
Rib screw |
85 Nm |
200 |
M10x50 |
Rib screw |
85 Nm |
280 |
M12x60 |
Hexagon head screw |
130 Nm |
350 |
M20x75 |
Hexagon head screw |
300 Nm |
420 |
M20x75 |
Hexagon head screw |
300 Nm |
Only for derailing protection device on END CARRIAGE of size 130 to 420
This work step only applies if the end carriage of size 130 to 420 has a derailing protection device.
Small side
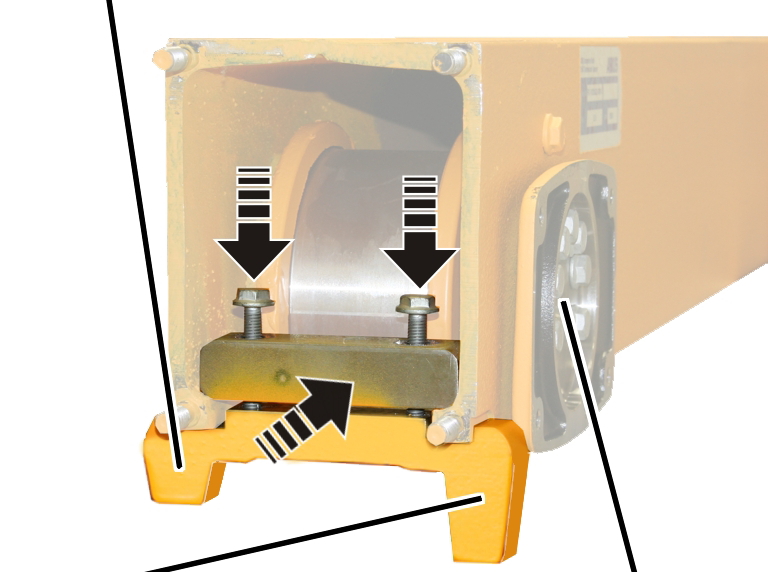
- Rotate the derailing protection device in such a way that the large side faces towards the crane travel drive.
- Insert the derailing protection device.
- Tighten screws (2x).
Wheel Ø |
Type |
Kind |
Tightening torque |
|---|---|---|---|
130 |
M8x45 |
Rib screw |
42 Nm |
160 |
M10x50 |
Rib screw |
85 Nm |
200 |
M10x50 |
Rib screw |
85 Nm |
280 |
M12x60 |
Hexagon head screw |
130 Nm |
350 |
M20x75 |
Hexagon head screw |
300 Nm |
420 |
M20x75 |
Hexagon head screw |
300 Nm |
Only with size 130 to 420
This work step applies only to end carriages of the sizes 130 to 420.
Buffer plate
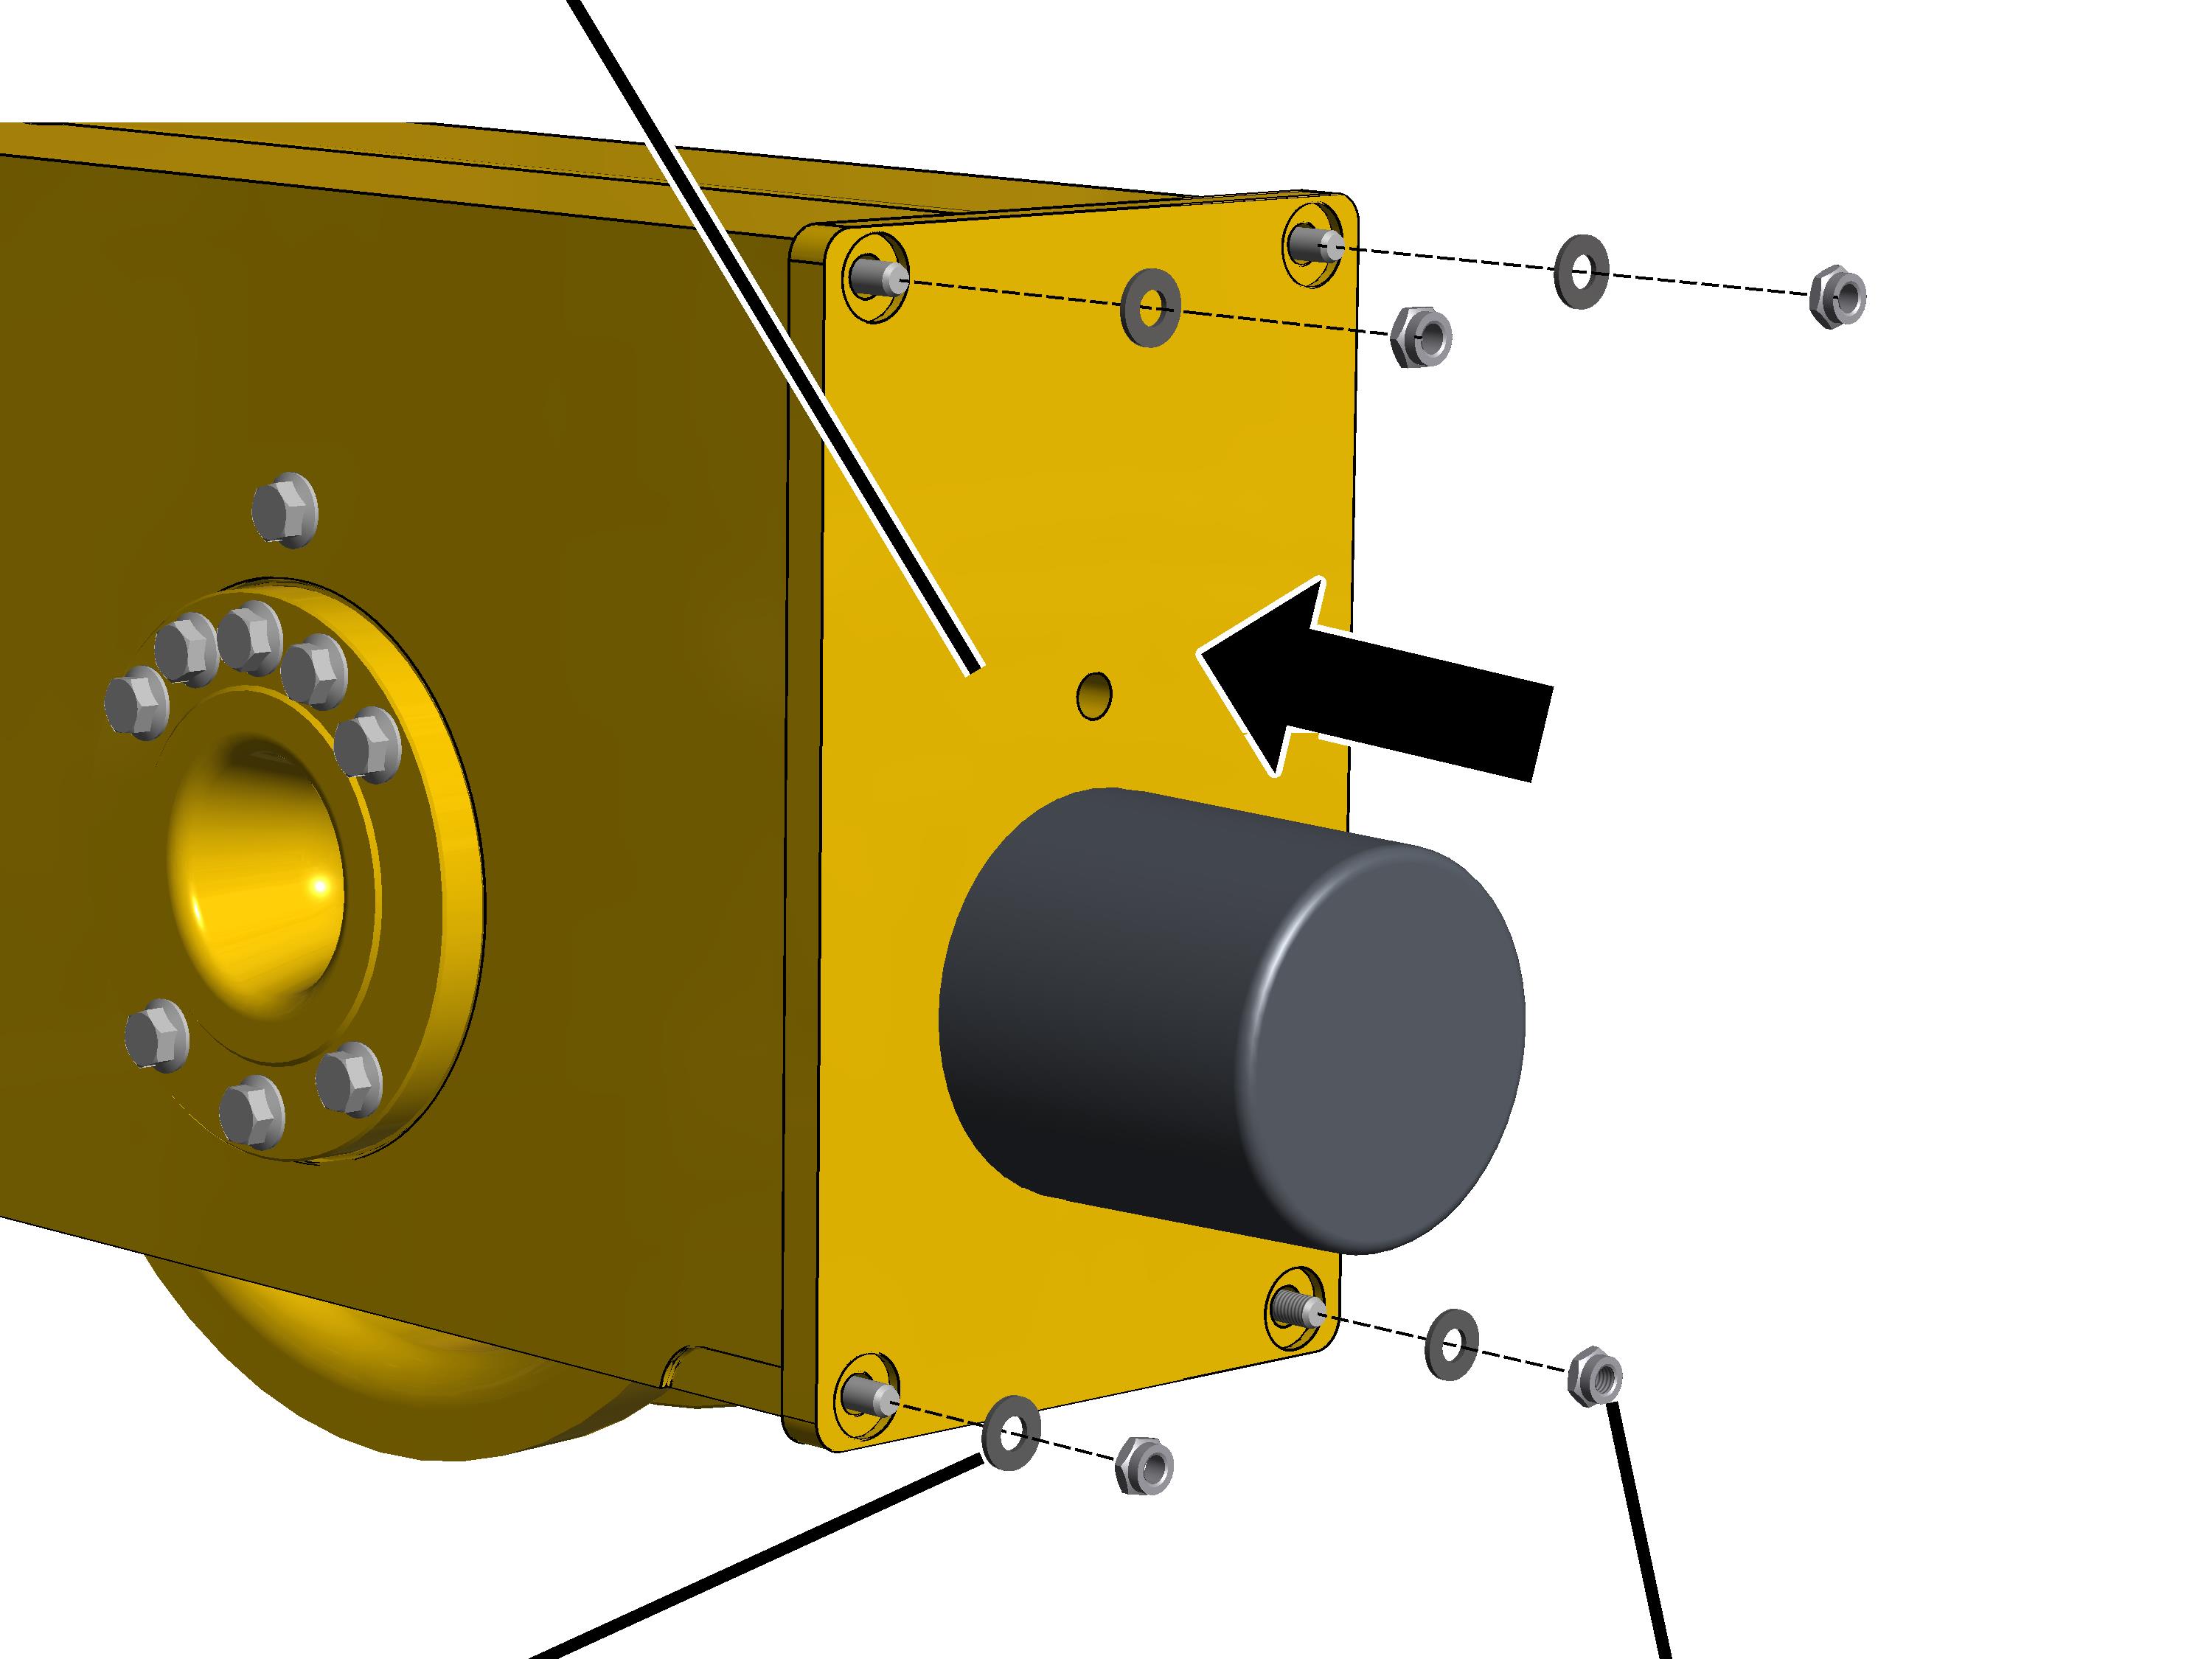
- Slide the buffer plate onto the threaded bolt.
- Size 160 to 420: fit the plastic washers (4x).
- Tightly screw the self-locking nuts M10 (4x). 6 Nm.
The self-locking nuts may only be reused maximally 3 times. After this, new self-locking nuts must be used.
Only with size 500
This work step applies only to end carriages of size 500.
Mounting plateHigh-tensile nut M16
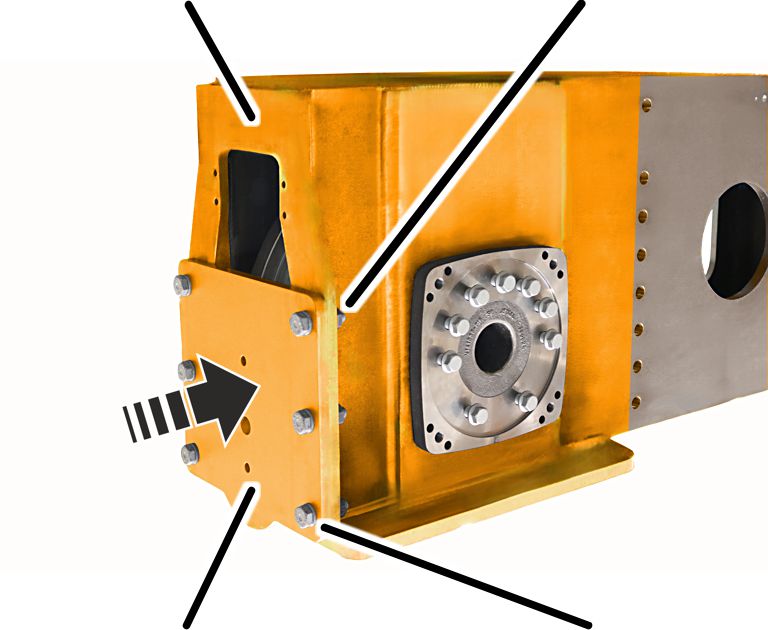
with washer 16
- Fit the washer 16 (6x) on high-tensile bolt M16x60 (6x) and screw buffer plate on mounting plate.
- Secure high-tensile bolt M16x60 (6x) with high-tensile nut M16 (6x). 250 Nm.
The high-tensile nuts may only be reused 3 times at most. After this, new high-tensile nuts must be used.
Only for guide rollers on END CARRIAGE of size 500
This work step only applies if the size 500 end carriage has guide rollers.
Hexagon head
screw M20x70High-tensile bolt M20x70 with washer 38/21x30
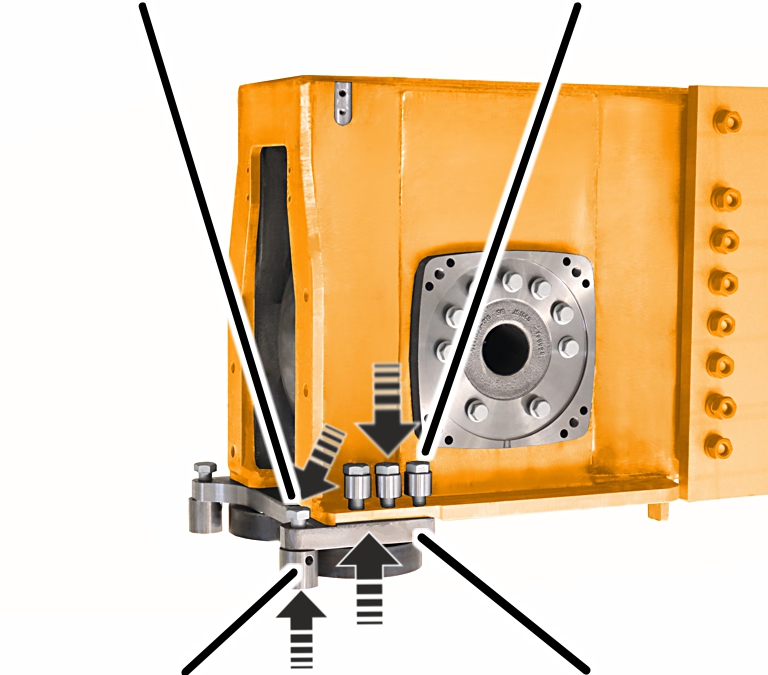
- Fit washers 38/21x30 (6x) on high-tensile bolts M20x70 (6x) and screw brackets on the end carriage on both sides. 450 Nm.
Here, the bevel must be positioned towards the screw head.
Installing the crane travel drive
- Determine the weight of the drive. See the ABUS Drive product manual.
- Secure the drive so that the weight can be held safely and the output shaft will not be subject to load (e.g. insert in round sling).
Bearing flange
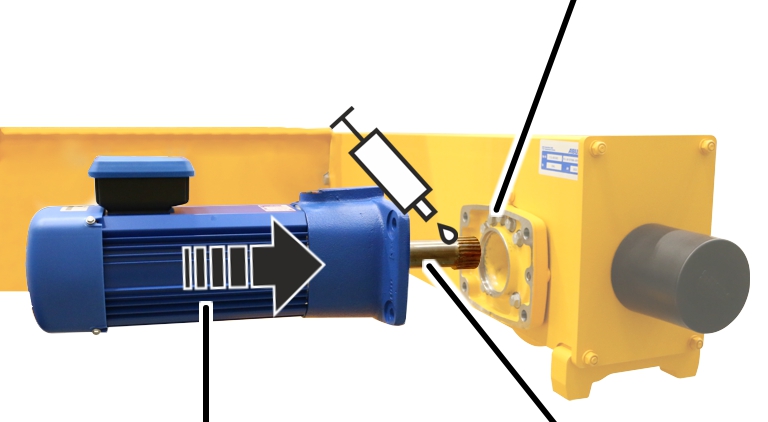
- Lubricate the gearing on the output shaft. Apply lubricant with brush to coat surface completely.
Lubricant: “High temperature paste PBC 1574”. See the ABUS Drive product manual for details.
- Push the drive into the wheel.
Only with AZP drives
This work step only applies when an AZP drive is to be mounted on the end carriage.
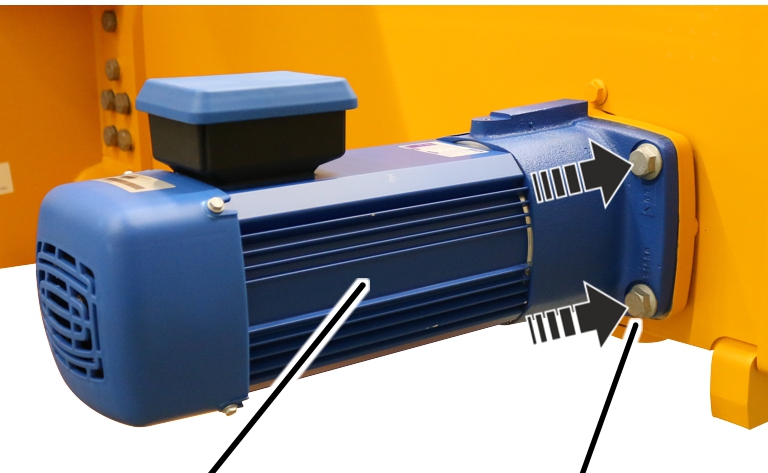
- Bolt on the drive with the rib screws (4x).
Size |
Type |
Tightening torque |
|---|---|---|
130 |
M8x25 |
35 Nm |
160 |
M10x30 |
75 Nm |
200 |
M12x30 |
115 Nm |
280 |
M16x40 |
300 Nm |
Only for crane travel drive AZF
This work step only applies if an AZF crane travel drive is to be mounted on the end carriage.
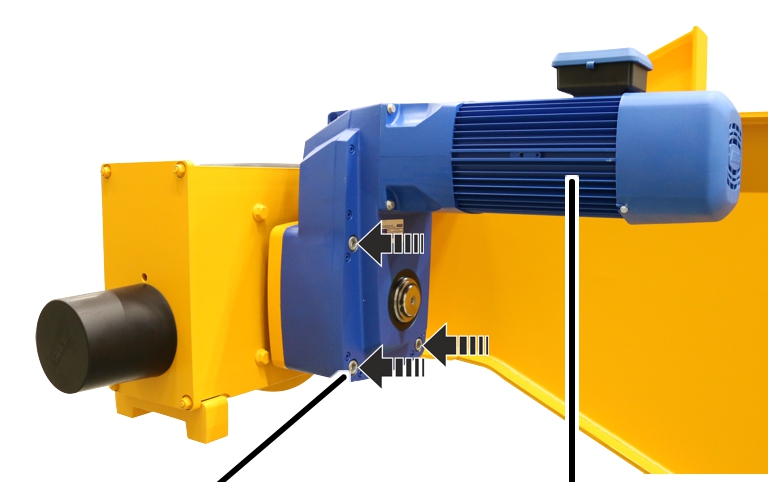
drive AZF
- Insert the crane travel drive in the wheel.
- Bolt on the crane travel drive with the fillister-head screws and washers (4x).
Size |
Type |
Tightening torque |
|---|---|---|
350 |
M12x100 |
85 Nm |
420 |
M12x100 |
85 Nm |
V420 |
M16x140 |
210 Nm |
V500 |
M16x140 |
210 Nm |
Disassembling the non-powered wheel
If the wheel is damaged or worn, it must be replaced by a new wheel.
The figures show the disassembly of a size 130 wheel. The removal of larger wheels does not essentially differ from this.
Preparing the crane
- Comply with occupational health and safety requirements.
- Prop up the end carriage close to the wheel.
Exposing the wheel
Only with size 130 to 420
This work step applies only to end carriages of the sizes 130 to 420.
Buffer plate
- Unscrew the self-locking nuts (4x).
- Remove the plastic washers (4x).
- Remove the buffer plate.
Only for guide rollers on END CARRIAGE of size 500
This work step only applies if the size 500 end carriage has guide rollers.
High-tensile bolt M20x70 with washer 38/21x30
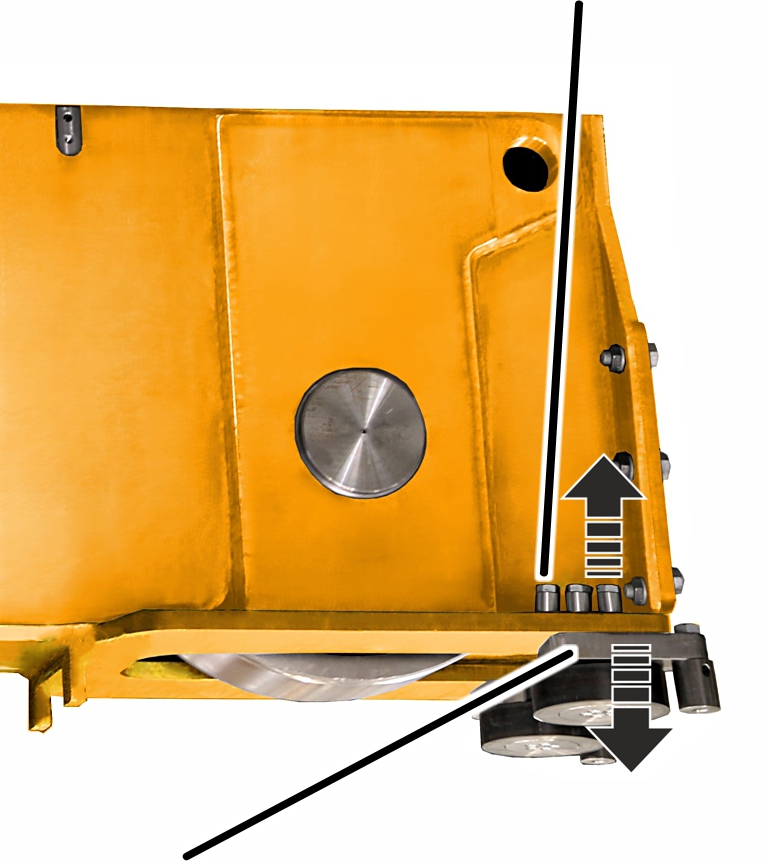
- Loosen high-tensile bolt M20x70 (3x) and remove bracket (1x) on both sides.
Only with size 500
This work step applies only to end carriages of size 500.
High-tensile
nut M16Mounting plate
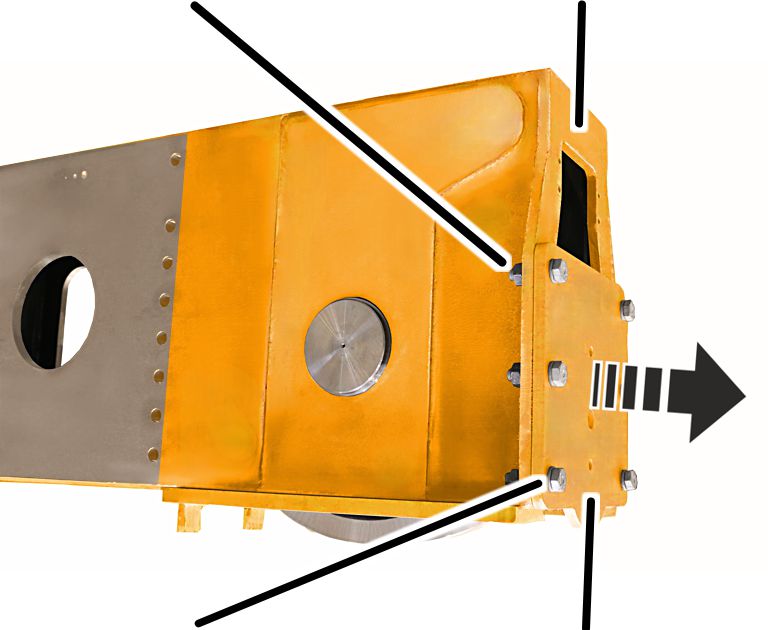
with washer 16Buffer plate
- Loosen high-tensile bolt M16x60 and remove the buffer plate from the mounting plate.
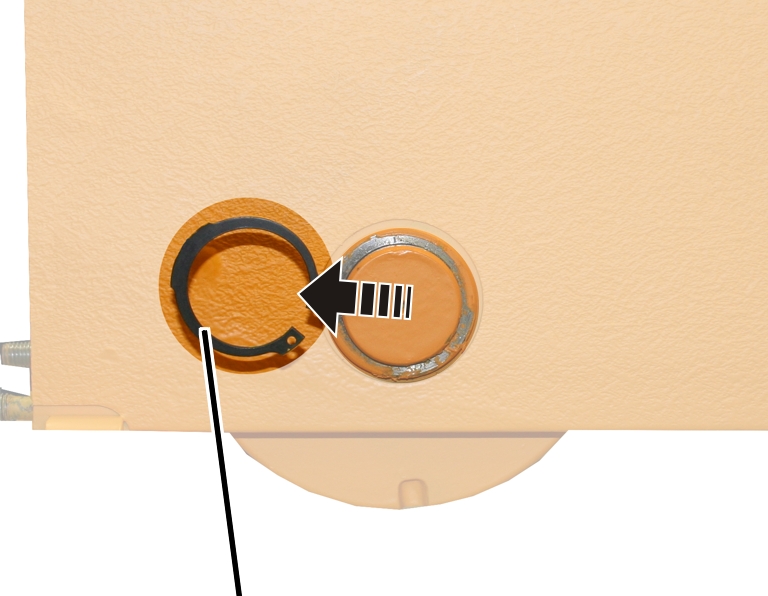
- Remove the circlip.
Only for guide rollers, derailing protection device on end carriages of the sizes 130 to 420
This section only applies if the end carriage has guide rollers of size 130 to 420 or a derailing protection device.
Screws
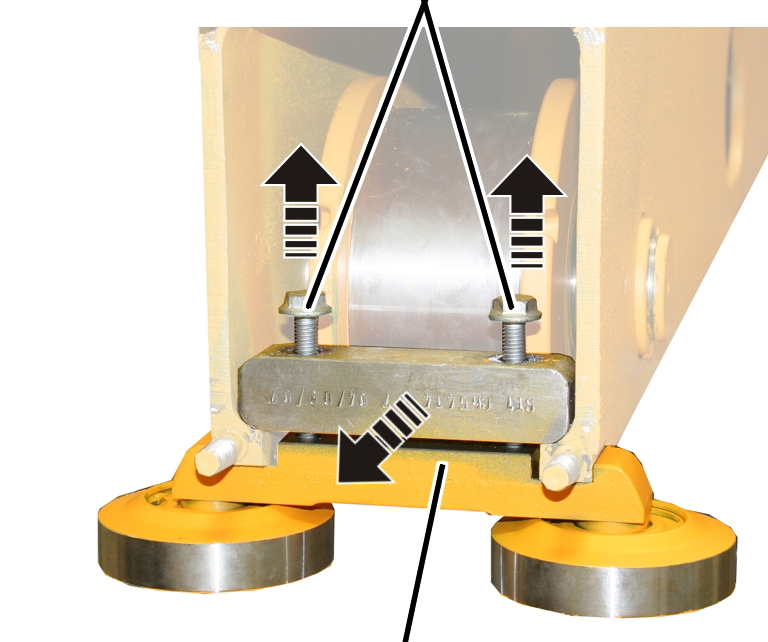
- Release screws (2x).
- Take out the bracket with guide rollers or derailing protection device.
Removing the wheel
Distance
bushBolt
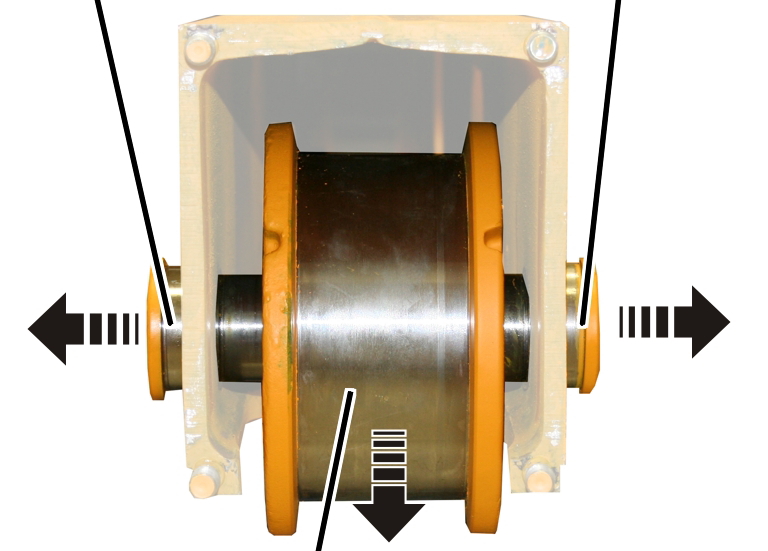
- Take out the bolt, distance bush and wheel.
Installing the non-powered wheel
If the wheel is damaged or worn, it must be replaced by a new wheel.
The figures show the installation of a size 130 wheel. The installation of larger wheels does not differ significantly.
Fitting the wheel
Distance
bushBolt
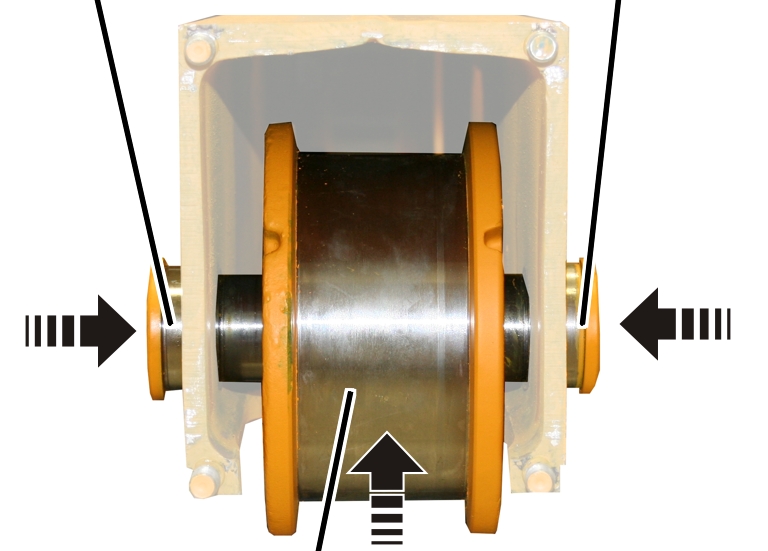
- Clamp the wheel in the end carriage. It does not matter which side faces inwards or outwards.
- Insert the bolt and distance bush. If necessary, lightly hammer the bolt and distance bush.
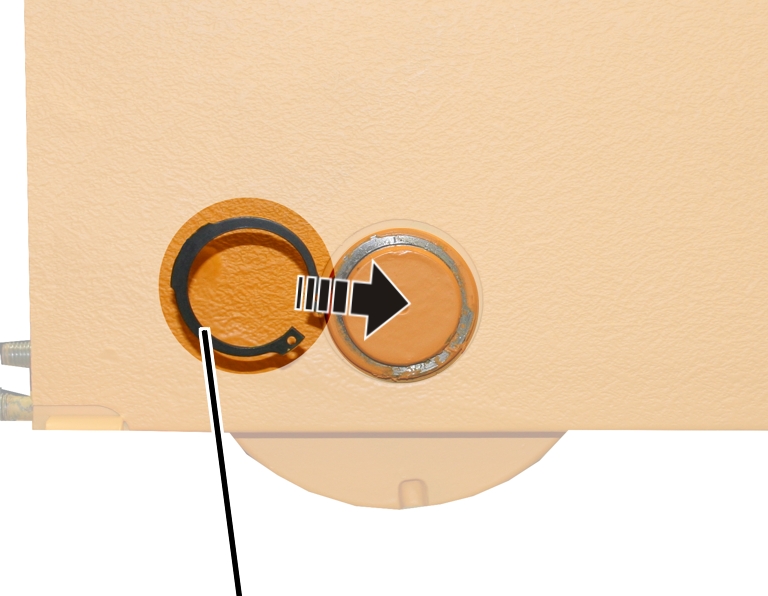
- Attach the circlip and neatly lock into place.
- Turn the wheel. It must move easily.
Only for guide rollers on end carriages of the sizes 130 to 420
This work step only applies if the size 130 to 420 end carriage has guide rollers.
Screws
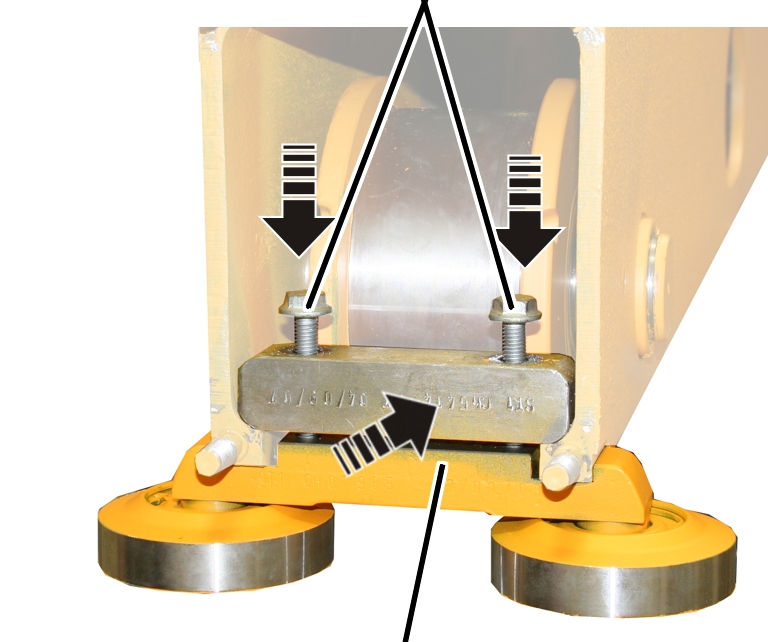
- Insert guide rollers.
- Tighten screws (2x).
Wheel Ø |
Type |
Kind |
Tightening torque |
|---|---|---|---|
130 |
M8x45 |
Rib screw |
42 Nm |
160 |
M10x50 |
Rib screw |
85 Nm |
200 |
M10x50 |
Rib screw |
85 Nm |
280 |
M12x60 |
Hexagon head screw |
130 Nm |
350 |
M20x75 |
Hexagon head screw |
300 Nm |
420 |
M20x75 |
Hexagon head screw |
300 Nm |
Only for derailing protection device on end carriage of size 130 to 420
This work step only applies if the end carriage of size 130 to 420 has a derailing protection device.
Small side
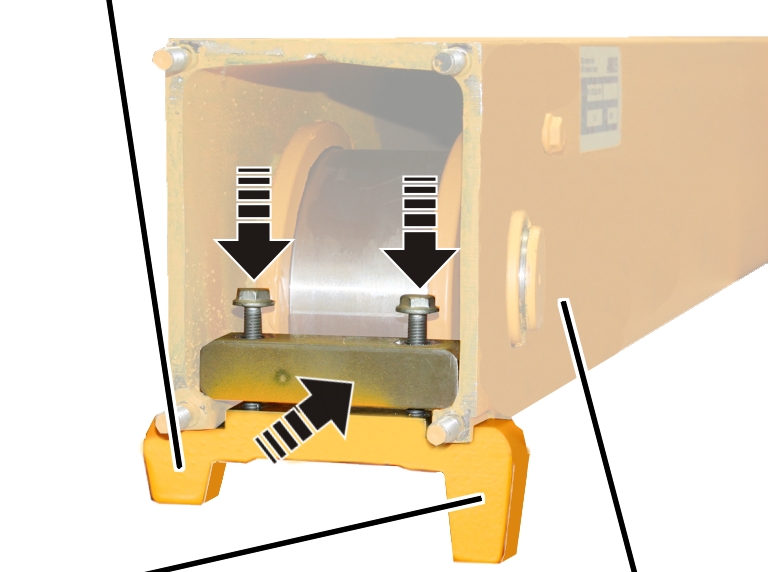
- Rotate the derailing protection device in such a way that the large side faces inwards (towards the crane travel drive).
- Insert the derailing protection device.
- Tighten screws (2x).
Wheel Ø |
Type |
Kind |
Tightening torque |
|---|---|---|---|
130 |
M8x45 |
Rib screw |
42 Nm |
160 |
M10x50 |
Rib screw |
85 Nm |
200 |
M10x50 |
Rib screw |
85 Nm |
280 |
M12x60 |
Hexagon head screw |
130 Nm |
350 |
M20x75 |
Hexagon head screw |
300 Nm |
420 |
M20x75 |
Hexagon head screw |
300 Nm |
Only for size 130 to 420
This work step applies only to end carriages of the sizes 130 to 420.
Buffer plate
- Slide the buffer plate onto the threaded bolt.
- Size 160 to 420: fit the plastic washers (4x).
- Tightly screw the self-locking nuts M10 (4x). 6 Nm.
The self-locking nuts may only be reused maximally 3 times. After this, new self-locking nuts must be used.
Only with size 500
This work step applies only to end carriages of size 500.
High-tensile
nut M16Mounting plate
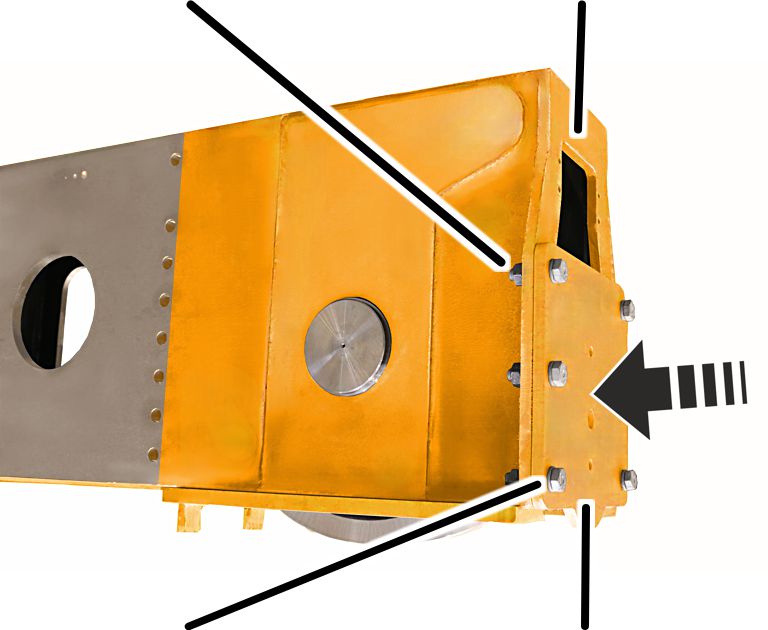
- Fit the washer 16 (6x) on high-tensile bolt M16x60 (6x) and screw buffer plate on mounting plate.
- Secure high-tensile bolt M16x60 (6x) with high-tensile nut M16 (6x). 250 Nm.
The high-tensile nuts may only be reused 3 times at most. After this, new high-tensile nuts must be used.
Only for guide rollers on end carriage size 500
This work step only applies if the size 500 end carriage has guide rollers.
High-tensile bolt M20x70
with washer
38/21x30Hexagon
head screw M20x70
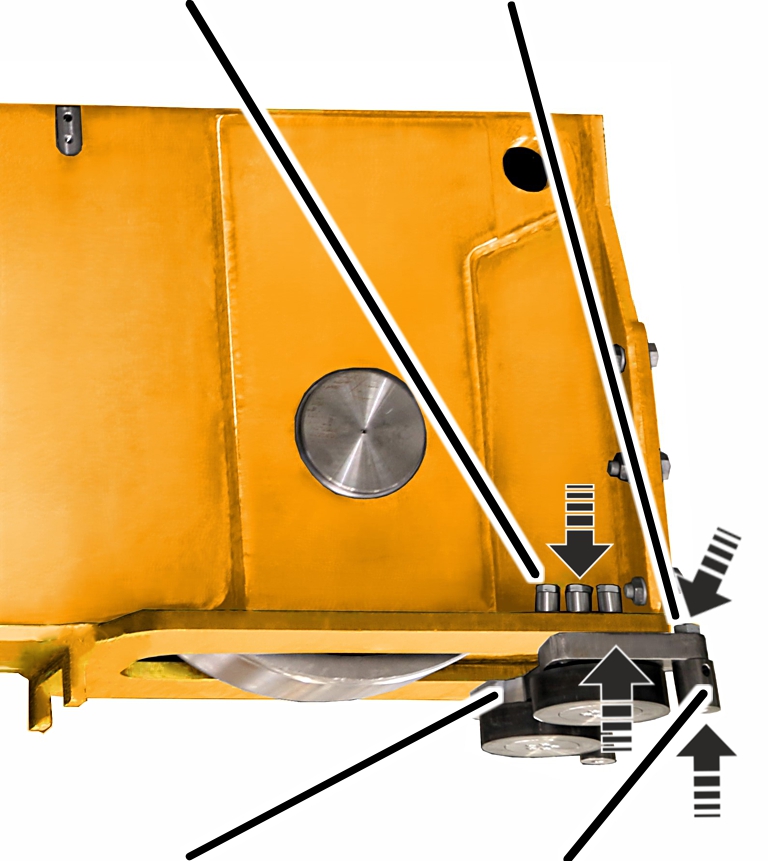
- Fit washers 38/21x30 (6x) on high-tensile bolts M20x70 (6x) and screw brackets on the end carriage on both sides. 450 Nm.
Here, the bevel must be positioned towards the screw head.
Screwing with tightening torque
Bearing bolt
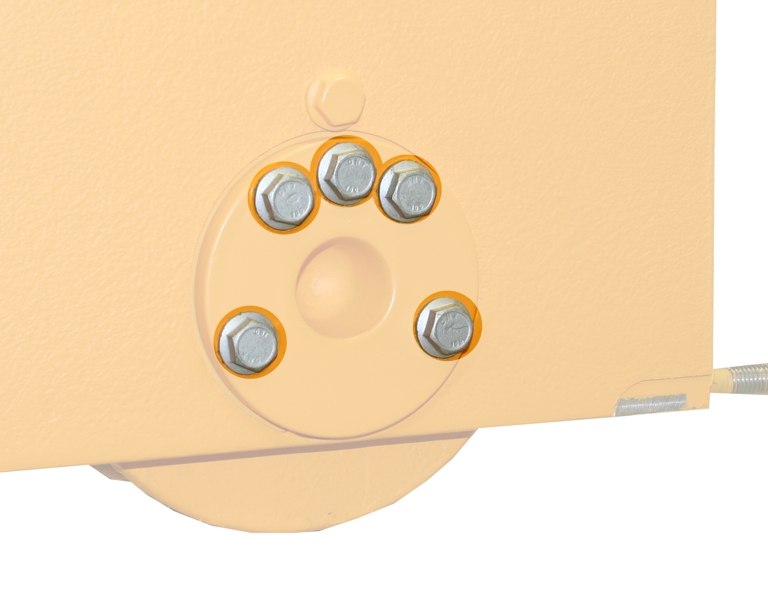
Size |
Type, size and length |
Number |
Tightening |
|---|---|---|---|
130 |
Rib screw M8x25 |
5x |
42 Nm |
160 |
Rib screw M8x25 |
5x |
42 Nm |
200 |
Rib screw M10x30 |
5x |
85 Nm |
280 |
Rib screw M12x40 |
5x |
130 Nm |
350 |
Rib screw M12x40 |
8x |
130 Nm |
420 |
Rib screw M16x40 |
8x |
330 Nm |
500 |
Rib screw M16x60 |
5x |
330 Nm |
Bearing flange
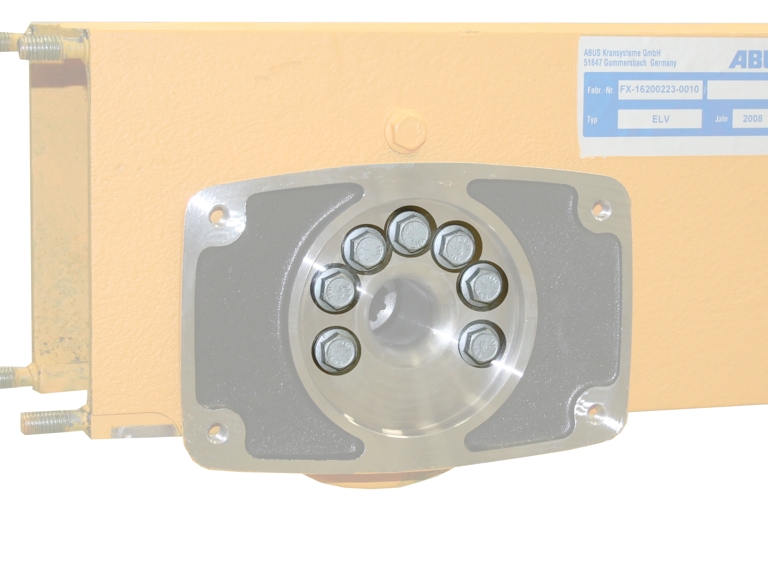
Size |
Type, size and length |
Number |
Tightening |
|---|---|---|---|
130 |
Rib screw M8x25 |
7x |
42 Nm |
160 |
Rib screw M8x25 |
7x |
42 Nm |
200 |
Rib screw M10x30 |
7x |
85 Nm |
280 |
Rib screw M12x40 |
7x |
130 Nm |
350 |
Rib screw M12x40 |
10x |
130 Nm |
420 with crane travel drive 420 |
Rib screw M16x40 |
10x |
330 Nm |
420 with crane travel drive 420 V |
Rib screw M16x70 |
10x |
330 Nm |
500 |
Hexagon head screw M16x60 |
9x |
300 Nm |
Guide rollers, clamping piece, derailing protection device of size 130 to 420
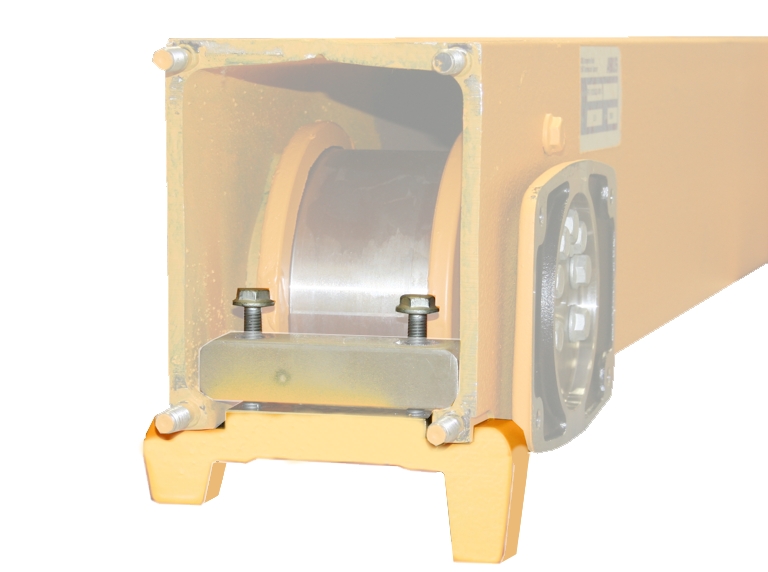
Size |
Type, size |
Number |
Tightening torque |
|---|---|---|---|
130 |
Rib screw M8x45 |
2x |
42 Nm |
160 |
Rib screw M10x50 |
2x |
85 Nm |
200 |
Rib screw M10x50 |
2x |
85 Nm |
280 |
Hexagon head screw M12x60 |
2x |
130 Nm |
350 |
Hexagon head screw M20x75 or M20x70 |
2x |
300 Nm |
420 |
Hexagon head screw M20x75 or M20x70 |
2x |
300 Nm |
Bracket size 500
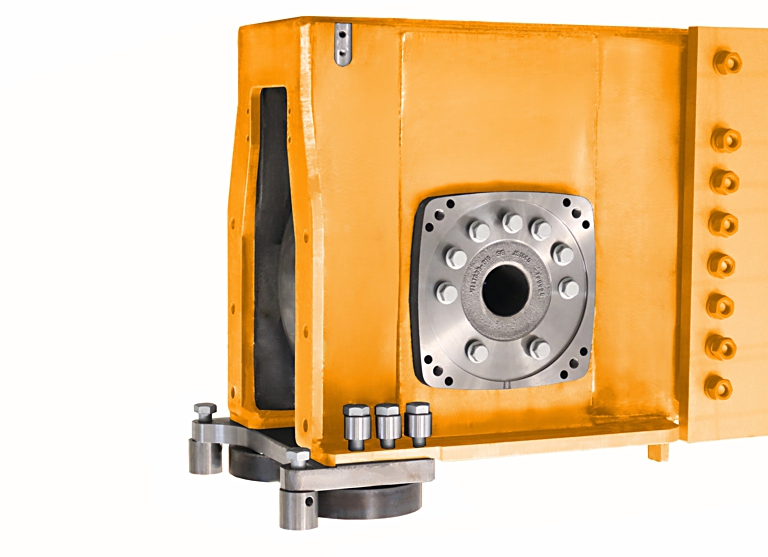
Size |
Type, size and length |
Number |
Tightening torque |
|---|---|---|---|
500 |
Hexagon head screw M20x70 with washer 38/21x30 |
3x |
450 Nm |
500 |
Hexagon head screw M20x70 |
1x |
450 Nm |
Buffer plate size 130 to 420
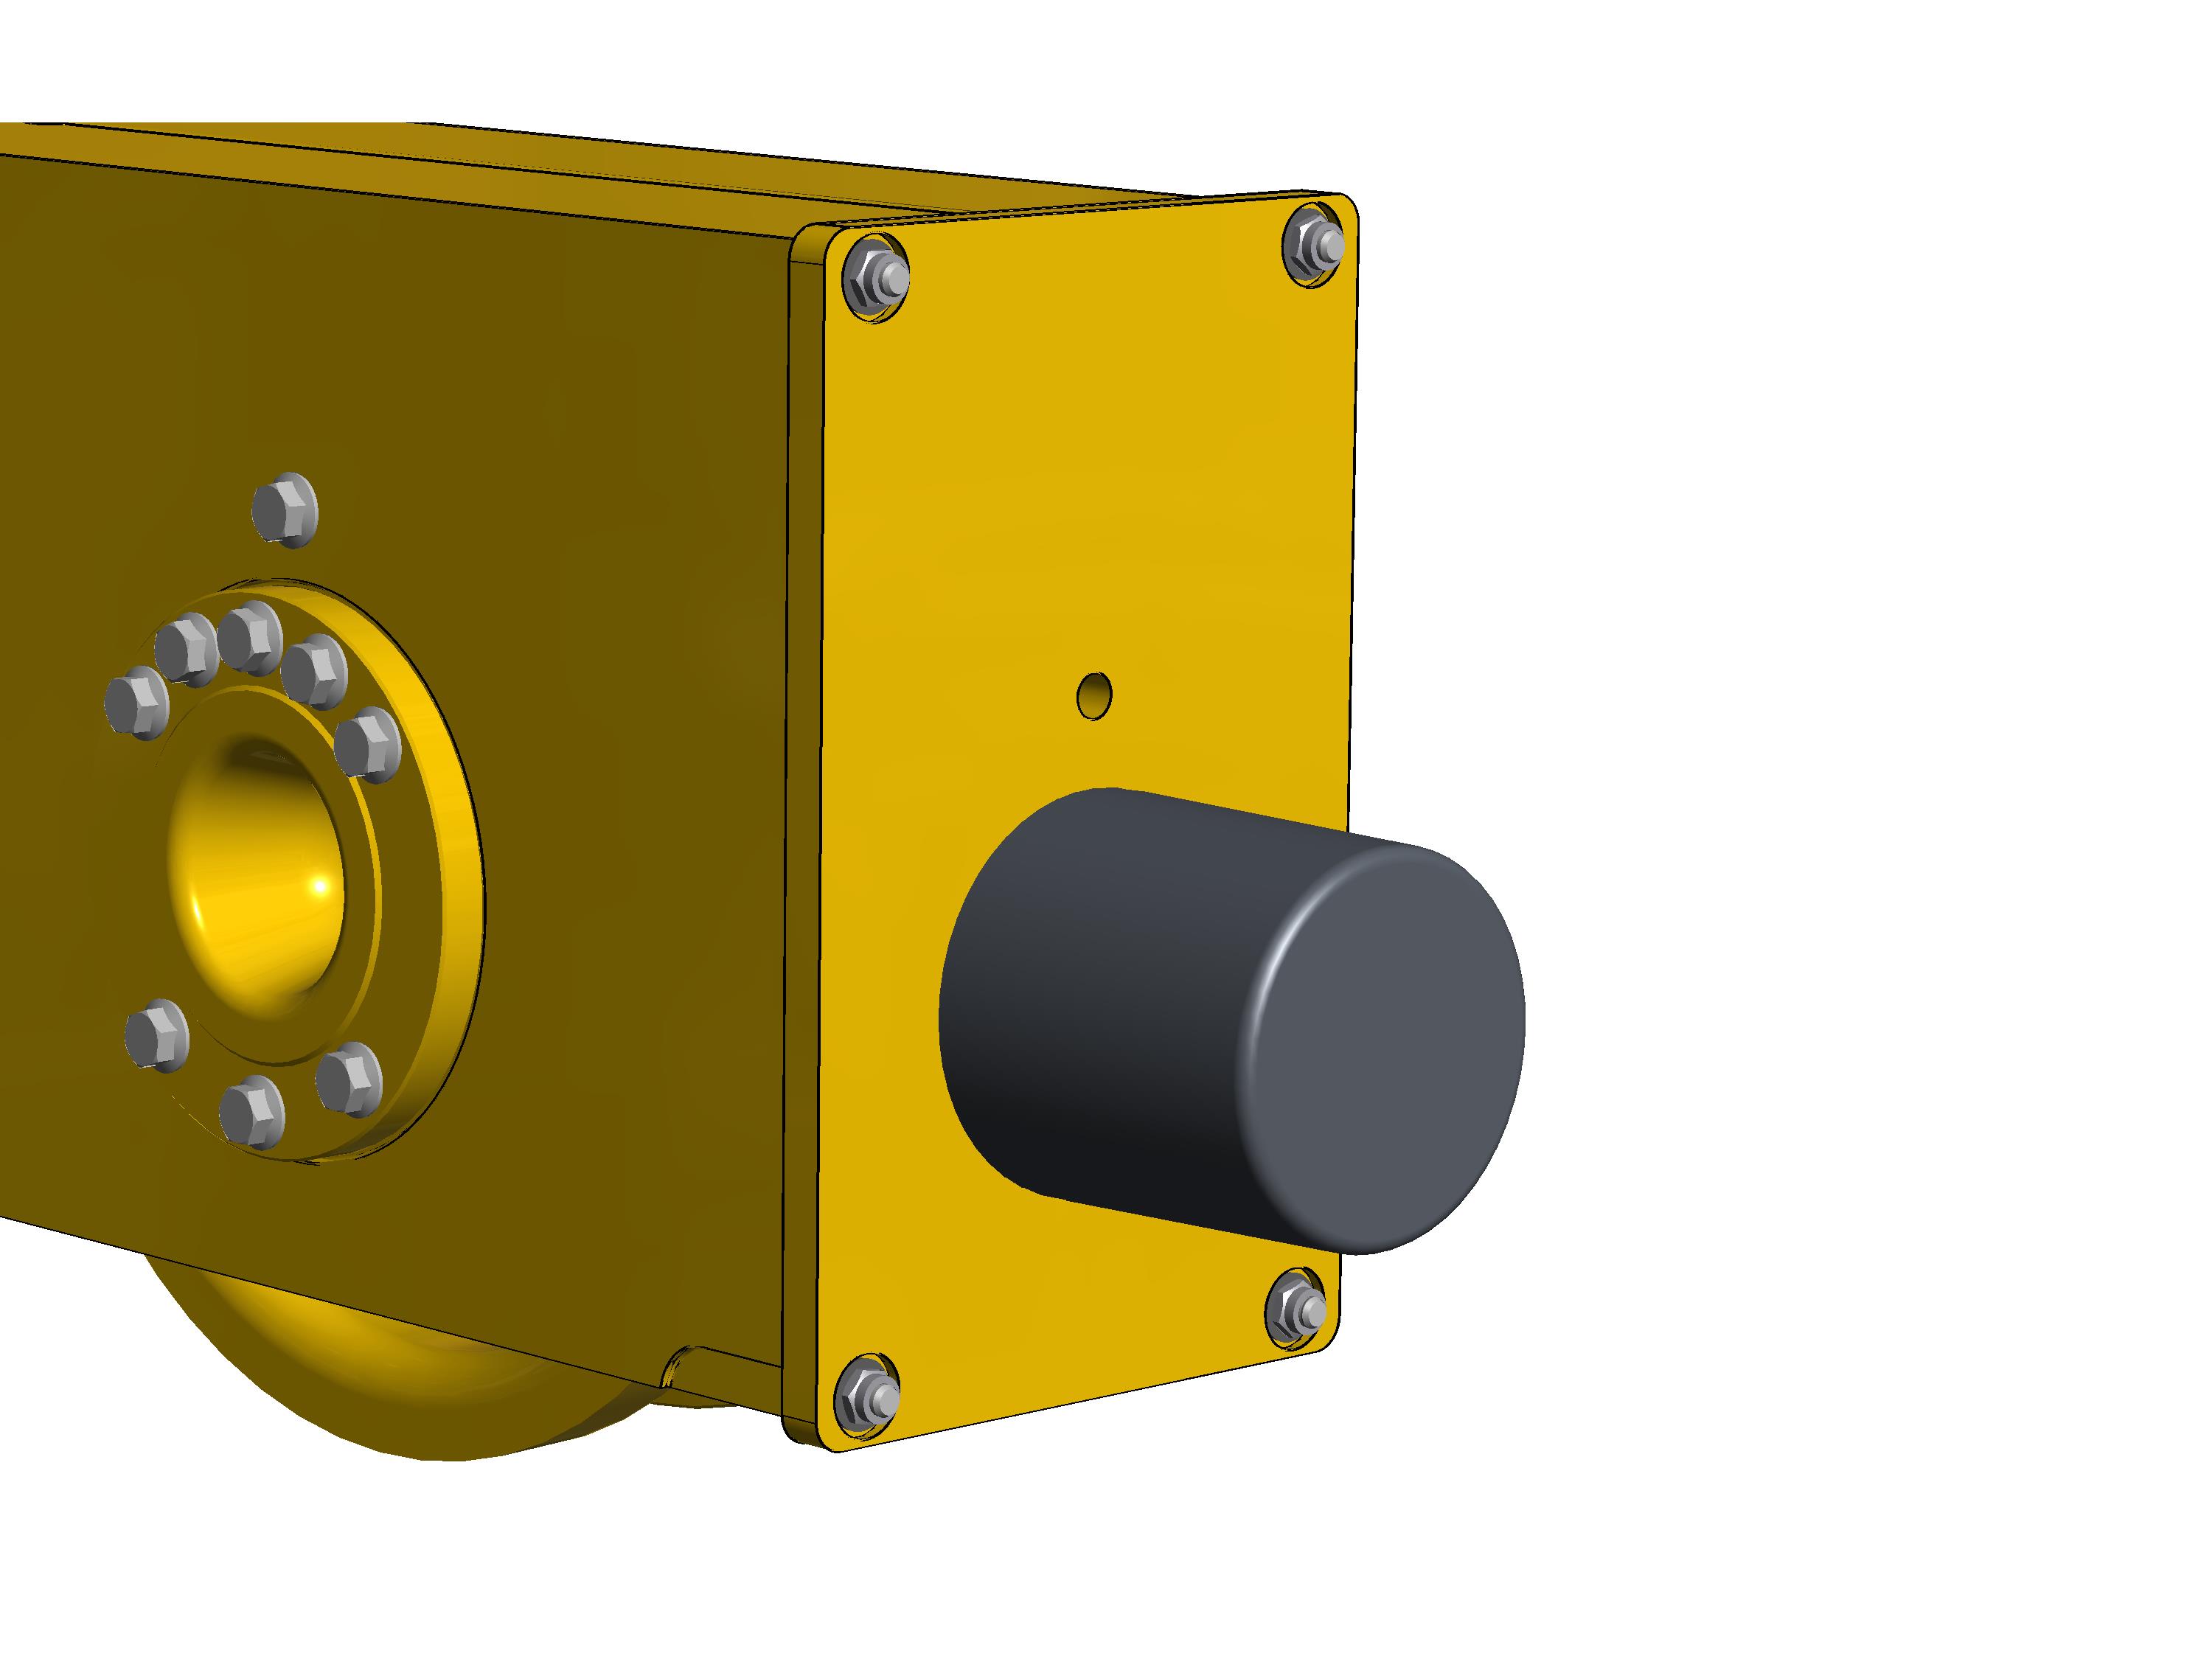
- Self-locking nut M10
- From size 160: Plastic washers
- 4x per buffer plate
- 6 Nm
Buffer plate size 500
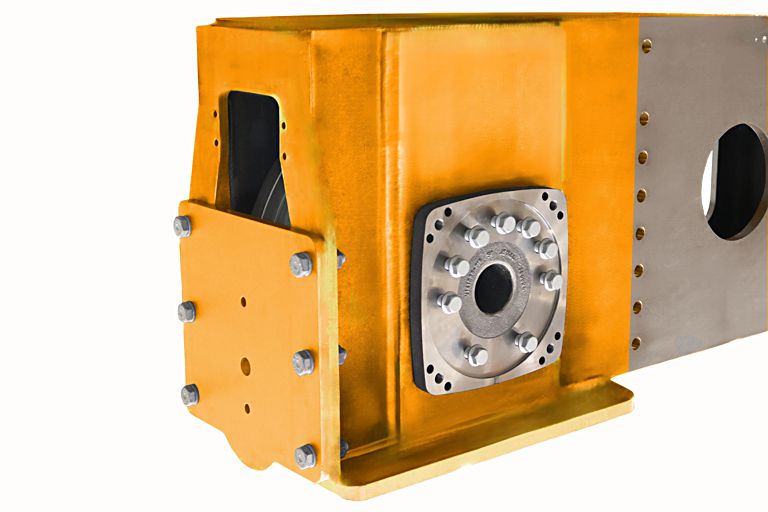
- High-tensile nut M16
- Washer 16
- 6x per buffer plate
- 250 Nm.
Size |
Type, size and length |
Number |
Tightening torque |
|---|---|---|---|
500 |
Hexagon head screw M16x60 with washer 16 |
6x |
250 Nm |
Crane travel drive AZP
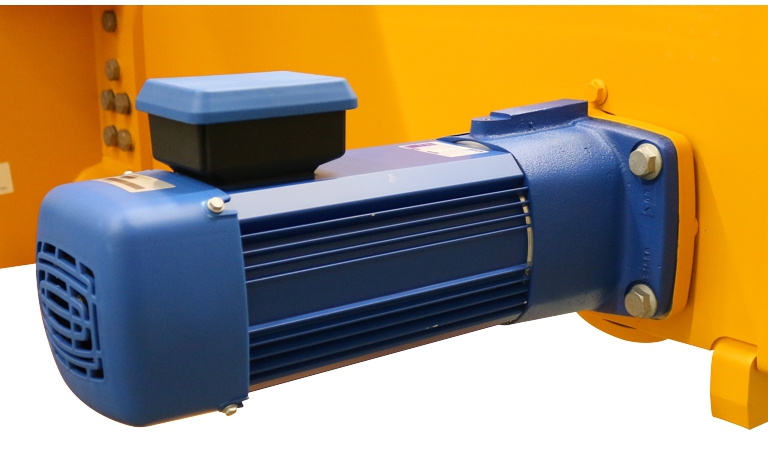
Size |
Type, size and length |
Number |
Tightening torque |
|---|---|---|---|
130 |
Rib screw M8x25 |
4x |
35 Nm |
160 |
Rib screw M10x30 |
4x |
75 Nm |
200 |
Rib screw M12x30 |
4x |
115 Nm |
280 |
Rib screw M16x40 |
4x |
300 Nm |
Crane travel drive AZF
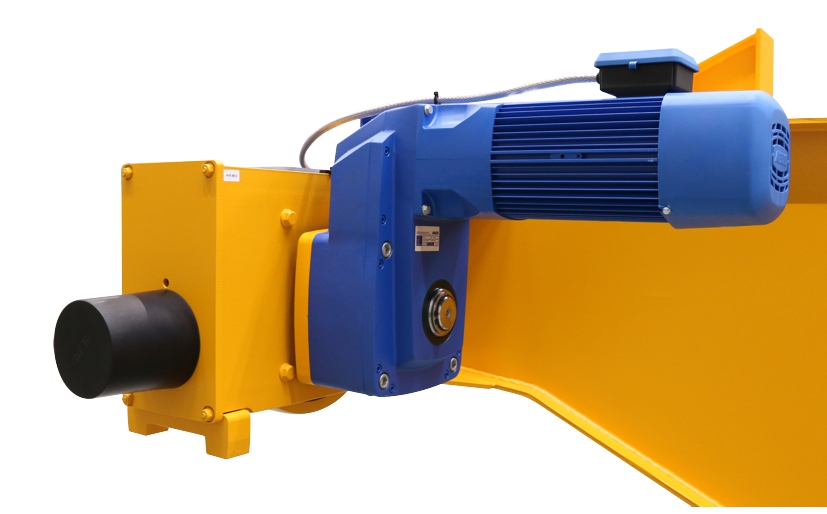
Size |
Type, size and length |
Number |
Tightening torque |
|---|---|---|---|
350 |
Fillister-head screw M12x100 |
4x |
85 Nm |
420 |
Fillister-head screw M12x100 |
4x |
85 Nm |
V420 |
Fillister-head screw M16x140 |
4x |
210 Nm |
V500 |
Fillister-head screw M16x140 |
4x |
210 Nm |
Lubricants
Only for guide rollers
Cylindrical roller bearings of the guide rollers
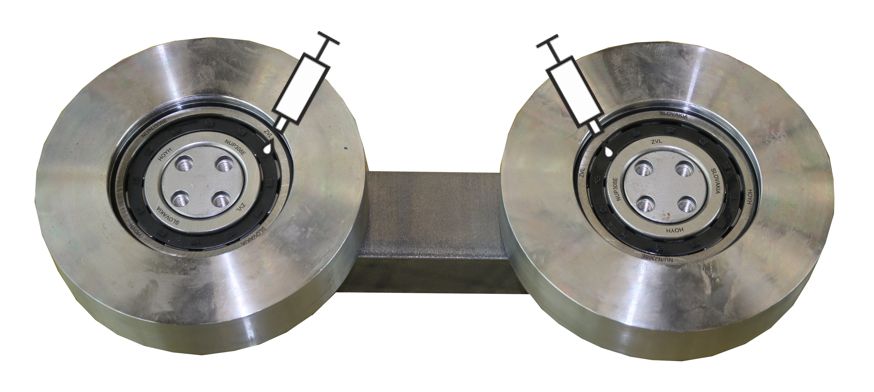
On-site lubrication with “High-Lub LT1 EP”, ABUS item number 318490.Lubrication ex works with “High-Lub LT1 EP”,ABUS item number 317880.
Lubricate the cylindrical roller bearing:
- When assembling or disassembling the guide roller
Only with wheel size 350, 420, 500
Self-aligning roller bearings in wheel
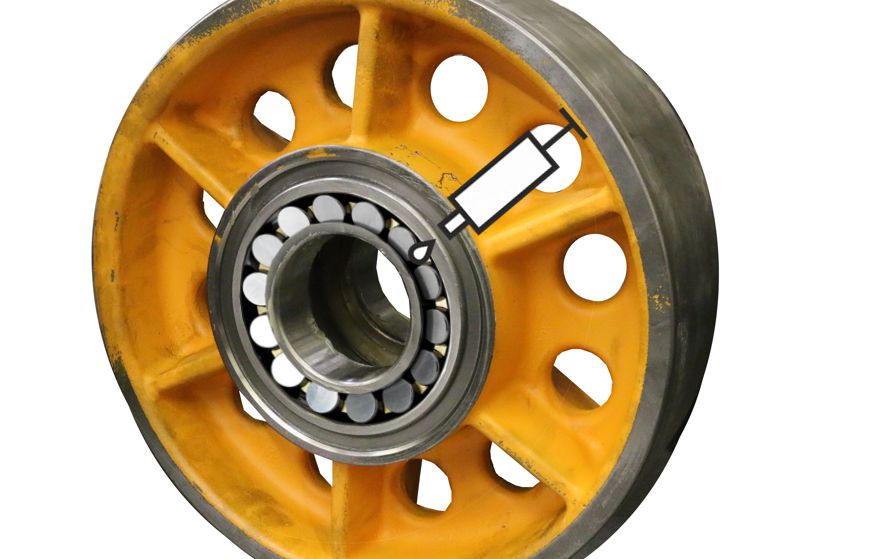
On-site lubrication with “High-Lub LT1 EP”, ABUS item number 318490.Lubrication ex works with “High-Lub LT1 EP”,ABUS item number 317880.
Lubricate the self-aligning roller bearing during:
- Assembly or disassembly of the wheel
For details, see “Disassembling the powered wheel”.
ABUS Service
Only in Germany
- If available, have the product number, serial number and customer number handy.
- Call the ABUS Service Centre:
- Phone: +49-2261-37-237
- If calling outside the usual business hours, leave a message on the answering machine.
- ABUS Service will return your call promptly.
- If necessary, send a description of the problem by fax or e-mail:
- Fax: +49-2261-37-265
- E-mail: service@abus-kransysteme.de
Only outside Germany
- Call the local ABUS branch or crane service partner.
Your local ABUS branch or crane service partner will provide details of contact data, contacts and availability.